Novel Cashew Nutshell Liquid-based
←
→
Page content transcription
If your browser does not render page correctly, please read the page content below
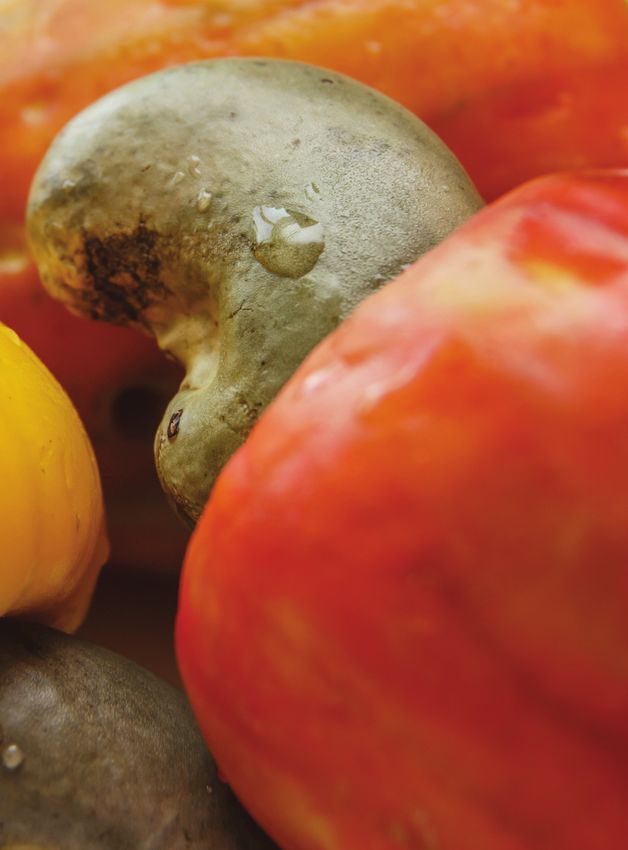
Novel Cashew
      Nutshell
 Liquid-based

      A team of Cardolite scientists
    expands its research on Cashew
 Nutshell Liquid-based waterborne
 epoxy curing agents with two new
agents in a range of direct-to-metal
       primer system formulations.

                                       © ADOBESTOCK | KULIKOVAN
Waterborne Curing Agents
Designed for High-Performance and
Low-VOC Protective Epoxy Coatings
Hong Xu, Joe Mauck, Fernanda Tavares, Anbu Natesh, and Jing Li,
Cardolite Corporation, USA

              A series of zero-volatile organic compound (VOC)            cure processes, and co-solvents upon film forma-
              waterborne epoxy curing agents based on cardanol,           tion, adhesion, and anti-corrosion performance are
              a non-food chain and renewable biomaterial, has             reviewed, and the challenges of improving long-term
              been developed to meet stricter regulation, as well         corrosion protection of waterborne primer systems
              as high-performance requirements. This article              over galvanized steel substrates are discussed.
              presents the latest performance studies of applying
              those new Cashew Nutshell Liquid-based waterborne
              curing agents in typical formulations for heavy duty,
                                                                          INTRODUCTION
              industrial, and transportation coatings applications.       Cashew Nutshell Liquid (CNSL) is a sustain-
              Test results revealed that the novel waterborne curing      able and non-food chain biomaterial that can be
              agents enable the formulations of low-VOC (< 75 g/L)        obtained as a byproduct of the cashew industry.1
              direct-to-metal primer systems with excellent perfor-       CNSL is contained in the honeycomb structure of
              mance, such as balanced fast cure and long pot life,        the cashew nutshell (Figure 1), and it is primarily
              superior adhesion, and long-term corrosion protec-          composed of 60% to 70% anacardic acid, 10% to
              tion of numerous metal substrates. Furthermore, the         20% cardols, 3% to 10% cardanols, and 2% to 5%
              influence of various solid epoxy dispersions, different     2-methylcardols.2

                    Figure 1—Cashew apple and nutshell.3

                                                           Cashew apple                                 Cashew kernel

                                                  Cashew nutshell                                    CNSL contained
                                                                                                     inside shell walls

                                                                                                     PAINT.ORG |                19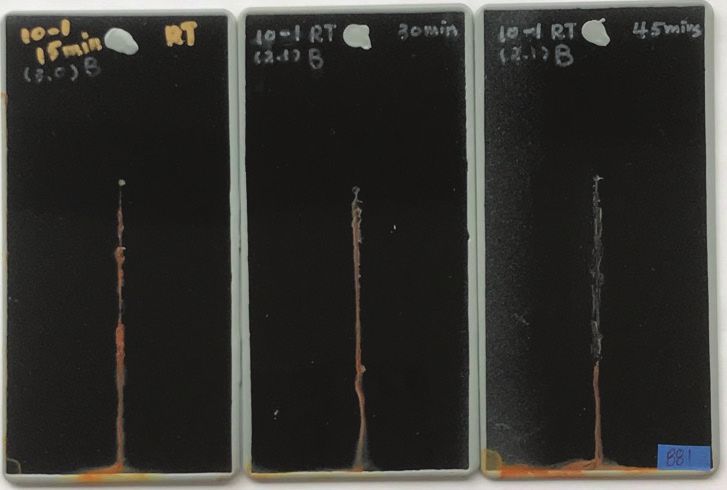
NOVEL CASHEW NUTSHELL LIQUID-BASED WATERBORNE CURING AGENTS

   Cardanol is the main component             substrates, a series of new-generation                         waterborne curing agent), of the first-gen-
derived from CNSL via decarboxylation         zero-VOC waterborne curing agents                              eration CNSL-based waterborne curing
and extraction.1 The chemical structure       has been recently developed. Some of                           agent, referred to as WB-C, and of a com-
of cardanol is a pentadecadienyl phe-         them are still CNSL-based with high                            mercial waterborne curing agent, referred
nol with a long aliphatic side chain that     bio-content, and some of them are syn-                         to as COM (a formulated polyamine
usually consists of a mixture of one, two,    thesized through non-CNSL processes to                         adduct-type waterborne curing agent) are
or three double bonds (Figure 2). The         expand end-use applications.                                   listed in Table 1 for comparison purposes.
unique and versatile structure of cardanol      This article presents the performance                           In this study, five types of solid epoxy
enables this natural oil to become a very     evaluation of two new waterborne curing                        dispersion resins, referred to as Resin
important chemical building block for         agents, one CNSL-based and one non-                            1, Resin 2, Resin 3, Resin 4, and Resin 5
numerous bio-based products. For exam-        CNSL type, used in several low-VOC                             were used. Their typical properties are
ple, phenalkamines and phenalkamides          waterborne primer systems. The ad-                             listed in Table 2.
are derived from cardanol and as a result,    vantages of these two new waterborne                              Linear dry time tests were carried
those products inherit some distinctive       curing agents, such as their ease of appli-                    out according to ASTM D5895-03. Clear
features that benefit the final coating or    cation, good anti-corrosion performance,                       (nonpigmented) coating systems were
adhesive systems: cardanol’s long aliphat-    adhesion to various substrates, and                            applied on 12 x 1 x 0.125 in. glass strips
ic side chain delivers excellent water re-    quick wet-on-wet recoat with polyure-                          via an 8-mil (200 μm) drawdown bar.
sistance (hydrophobicity), flexibility, and   thane (PU) are reported. Furthermore,                          The glass strips were immediately placed
low viscosity; its aromatic ring provides     the influences of varying solid epoxy                          on drying recorders that had been stored
good chemical resistance; its phenolic        dispersions, stoichiometric ratios, and                        in a 25°C incubator. The styluses were
hydroxyl contributes to excellent adhe-       co-solvents on the final performance of                        lowered onto the wet coating to start the
sion to various substrates, as well as fast   waterborne coating systems are discussed.                      linear dry time tests.
ambient and low-temperature cure.4                                                                              The waterborne primer systems were
   Traditionally, phenalkamines and                                                                          applied over different types of substrates
phenalkamides are used in solventborne
                                              MATERIALS AND EXPERIMENTAL                                     via air spray. After a seven-day room tem-
and high solids epoxy coating systems in      The typical properties of two new                              perature (RT) cure or bake in a 60°C oven
marine and protective coating applica-        waterborne curing agents, referred to                          for one to two hours, the panels were evalu-
tions.4 To meet more stringent govern-        as WB-A (a modified polyamine-type                             ated for adhesion tape tests (ASTM D3359)
ment regulations and the increasing           waterborne curing agent) and WB-B                              and salt-spray exposure (ASTM B117).
requests for renewable and sustainable        (a CNSL-modified polyamine-type
products, a series of zero-VOC water-
borne CNSL-based curing agents was
developed by stabilizing the cardanol-               TABLE 1—Waterborne Curing Agents–Typical Properties
based structures in water without the
help of co-solvents.5 Those waterborne                        PROPERTIES                        WB–A      WB–B              WB–C             COM
CNSL-based curing agents not only have                  Viscosity at 25°C (cPs)                 5600       10798         15000–55000      12000–20000
high bio-content (41%~55%),6 but also                   Amine value (mg KOH/g)                   204        277            140–180           170–210
retain the unique performances from sol-
                                                        Solids (%)                               80          80               50                80
ventborne phenalkamine counterparts,
such as fast cure, good early water resis-              AHEW (amine hydrogen                    165         144                 270           150
                                                        equivalent weight)
tance, excellent adhesion to various sub-
strates, and high mechanical strengths.5                Color (Gardner)                          8          10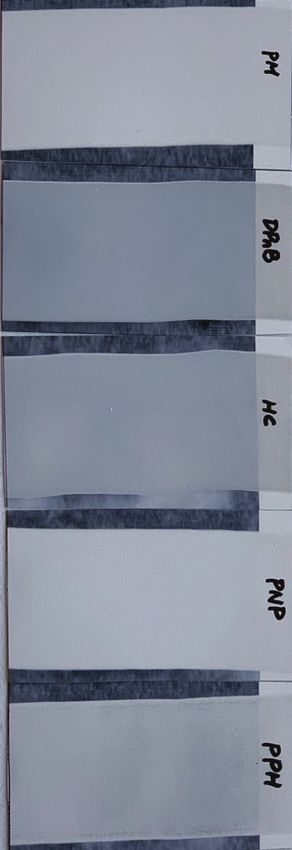
FIGURE 3—Viscosity changes of waterborne curing agents as function of the percentage
of added water.
RESULTS AND DISCUSSIONS 40000
Part I: Improved Application 35000
Properties From New Waterborne 30000
Curing Agents
Viscosity / cPs
25000
WB-A
WB-C is part of the first generation of 20000
CNSL-based waterborne curing agents, WB-B
15000
and it has 44.1% calculated bio-content. WB-C
In previous studies, 5,6 WB-C systems 10000
exhibited very interesting properties, COM
5000
such as fast cure, excellent early water
resistance, and excellent compatibility 0
0 5 10 15 20 25 30
with various epoxy resins. However,
WB-C systems needed further improve- Water added by wt%
ments on some application properties,
such as an ability to be easily diluted by
water and a more balanced cure speed FIGURE 4—Dilution properties of WB-A with various solid epoxy dispersions.
and pot life. WB-A and WB-B are the
latest high-performance waterborne 25000
curing agents to be developed. WB-A
Viscosity of mixture (cPs)
is not based on CNSL, while WB-B is 20000
CNSL-based with 44.0% calculated
bio-content. In Table 1, it can be seen 15000
that, even though WB-A (5600 cPs) and
10000
WB-B (10798 cPs) curing agents are sup-
plied at 80% solids, they still have much 5000
lower viscosities than 50% solids WB-C
(15000–55000 cPs). The viscosities of 0
WB-A and WB-B are also lower than 0 5 10 15 20 25 30 35 40 45
that of a commercial product, COM. Water added by wt%
If the initial solids differences of
the four waterborne curing agents are Resin 1 Resin 3 Resin 4
ignored and the focus is on the viscos-
ity changes of each waterborne curing
agent after adding a certain percentage FIGURE 5—Linear dry time data of various waterborne systems.
of water, it can be seen in Figure 3 that
WB-A and WB-B exhibit improved 4 4
dilution properties: only 10% water 3.5
could lower the viscosities of WB-A and 3
Dry-hard 3me @ 25oC / h
3
WB-B from 6300 cPs and 14700 cPs to
2
4200 cPs and 10000 cPs, respectively; 2.5
while the viscosity of WB-C system was
Pot life (h)
2 1
kept around 20000 cPs after adding 25%
water. The results suggest that the two 1.5
0
new waterborne curing agents are more 1
application-friendly. -1
It is common for a waterborne curing 0.5
agent to have different initial viscos- 0 -2
ities when mixed with various solid WB-A WB-B WB-C COM
epoxy dispersion resins. For example,
the initial viscosities of WB-A mixed Resin 1 Resin 3 Pot life
with Resin 1, Resin 3, and Resin 4 (at
stoichiometric ratio) were 9650 cPs,
14920 cPs, and 21250 cPs, respectively, to less than 2,000 cPs. Even in the case It is always desirable that a paint
as shown in Figure 4. Regardless of the of the high admixture viscosity of WB-A system exhibits fast-cure performance
resin selected, the dilution results indi- with Resin 4, 20% extra water could while having a long work window (pot
cate WB-A-based systems can be easily effectively reduce viscosity to around life) for easier application, though this
diluted to low viscosities with small 3000 cPs. This good dilution property is usually a difficult task to accomplish.
amounts of water. Less than 15% extra of WB-A suggests that WB-A is suitable For example, CNSL-based WB-C curing
water was enough to bring admixture for high solids (>60% solids) waterborne agent has excellent fast-cure properties
viscosities of WB-A with Resin 1 and 3 formulations. (less than 2 h of dry-hard time at 25°C)
PAINT.ORG | 21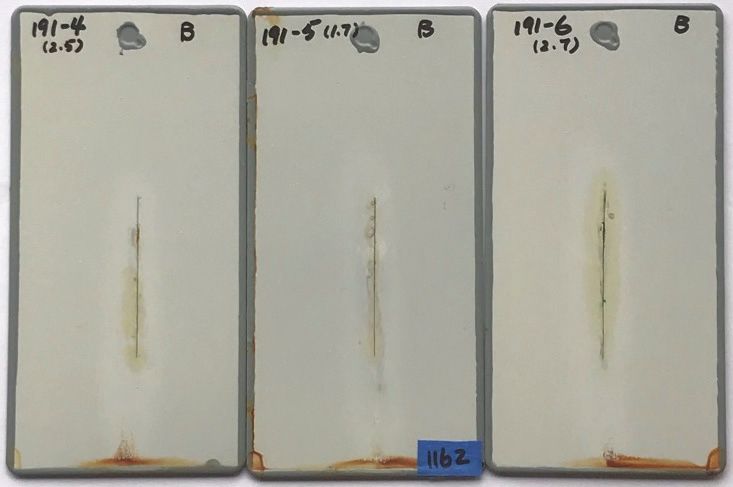
NOVEL CASHEW NUTSHELL LIQUID-BASED WATERBORNE CURING AGENTS
with various solid epoxy dispersion In Table 3, the formulations of three formulated with the same solid epoxy
resins. However, as shown in Figure low-VOC waterborne primer systems, dispersion (Resin 3), at similar solids
5, its average pot life is around 1.5 h MC #1, MC #2, and MC #3, were listed (around 57%), with comparable pig-
(displayed as red dot), which can be based on WB-A, WB-B, and WB-C cur- ment volume concentration (PVC from
considered short for some applications. ing agents, respectively. For comparison 27% to 30%), and using the same 1.25
Through better design of the polymers’ purposes, all three primer systems were stoichiometric ratio. It can be seen that
structures, new waterborne curing
agents WB-A and WB-B exhibit the
TABLE 3—Waterborne Primer Formulations Based on WB–A, WB–B, and COM
improved properties with fast cure and
longer pot life. As indicated in Figure 5, COMPONENTS MC #1/WB-A MC #2/WB-B MC #3/COM
WB-A and WB-B could achieve dry- WB-A 5.70 – –
hard times of 3 h or less with both Resin
WB-B – 4.79 –
1 and Resin 3 while providing extended
pot lives of 3.5 h. The competitive-based COM – – 5.47
system (COM) also shows long pot life Rheological additive (BENTONE SD-2) 0.08 0.08 0.08
but was slower in dry-hard times. Defoamer (BYK1640) 0.08 0.08 0.08
The Persoz hardness data from Figure Pigment 1 (Ti-Pure R-706) 3.57 3.63 3.42
6 confirm that WB-A and WB-B systems
Pigment 2 (Cimbar EX Barium Sulfate) 7.85 7.99 7.53
deliver faster hardness development than
COM-based systems. Moreover, the fast- Inhibitor 1 (HALOX SW-111) 6.42 6.53 6.16
cure properties of WB-A and WB-B could Inhibitor 2 (HALOX 550WF) 0.43 0.44 0.41
benefit wet-on-wet topcoat applications, Filler 1 (Zeeospheres G 200) 4.28 4.36 4.11
as presented in detail later in this article. Filler 2 (WOLLASTOCOAT 10 ES) 8.56 8.71 8.21
Filler 3 (Mica WG-325) 0.50 0.51 0.48
Part II: Waterborne Primer/Mid-coat
Solvent 1 (DOWANOL PM) 1.71 1.74 1.64
Systems Based on New WB-A and
Solvent 2 (DPnB) 0.29 0.29 0.27
WB-B Curing Agents
Flash rust inhibitor (HALOX Flash-X 150) 0.21 0.22 0.21
Excellent long-term corrosion protec-
Water 10.35 10.53 9.92
tion is a key property required in water-
borne epoxy primer systems and mid- Subtotal of Part A 50.04 49.90 47.99
coat systems; however, it is also the most Resin 3 40.68 39.21 43.11
challenging to achieve. In this study, Water 9.28 10.89 8.90
newly developed WB-A and WB-B Subtotal of Part B 49.96 50.10 52.01
curing agents were evaluated to assess
Total Part A & B 100.00 100.00 100.00
their anti-corrosion performance after
extended salt-spray exposure. Different VOC (g/L) 69.17 72.41 65.76
performance aspects, such as rust or wt% NVM 57.50 56.54 57.32
blisters on field, and creep along the wt% Pigment 31.19 31.73 29.91
scribe line, were checked after certain vol% NVM 45.74 44.27 46.04
exposure intervals, and wet adhesion
% PVC 28.51 30.00 26.96
was also conducted on the test panels
after 800 h of salt-spray exposure. Epoxy/amine 1.25 1.25 1.25
FIGURE 7—Panel images of WB-A/MC #1, WB-B/MC #2 and COM/MC #3
FIGURE 6—Persoz hardness development of various waterborne systems.
systems after 1162 h, 949 h, and 1162 h of salt-spray exposure, respectively
(SA 2.5 steel substrate, bake cure, DFT ≈ 60–75 μm).
400
Persoz Hardness (sec)
WB-A WB-B COM
300
200
100
0 72h
WB-A WB-B
WB-C COM 24h
WB-A WB-B
Resin 1 WB-C COM
Resin 3
24h 48h 72h 168hr
22 | MAY 2020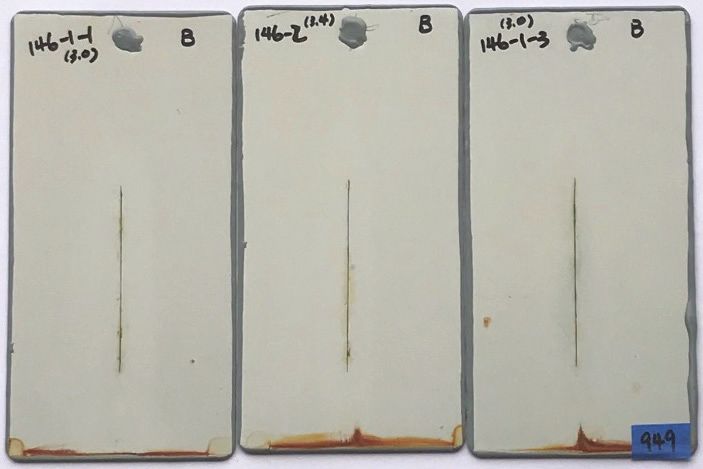
VOC values for those waterborne primer                       As part of this study, one can also             creeps developed with the widths of 3
  systems are less than 75 g/L.                             notice the significant impact of film              mm, 1.5 mm, and 3.5 mm for MC #1, MC
     The anti-corrosion performances of                     thickness on long-term anti-corrosion              #2, and MC #3 systems, respectively.
  MC #1, MC #2, and MC #3 formulations                      performance, especially over sand-                 These test results indicate the new water-
  were assessed in direct-to-metal (DTM)                    blasted panels. For example, MC #1                 borne primer systems could provide very
  primers. Those primer systems were                        formulation was applied to panels at               good corrosion protection on CRS, but it is
  directly air sprayed to various nonpre-                   various DFT of 37 μm, 50 μm, 65 μm, and            still a major challenge to achieve superior
  treated metal substrates, such as SA 2.5                  100 μm, and then exposed in the salt-              adhesion to steel substrates with a smooth
  blasted steel panels, cold rolled steel                   spray chamber. After 500 h of salt-spray           surface profile after long-term salt-spray
  (CRS) panels, galvanized steel panels,                    exposure, the system with 37 μm DFT                exposure.
  aluminum alloy AA 2024 T3 panels,                         already showed severe rust and blisters,              Next, this study evaluated the
  and stainless steel panels. Two cure                      while the other three systems still had            anti-corrosion and adhesion properties
  conditions were used for those water-                     intact films; up to 1100 h, the system with        of the new waterborne curing agents on
  borne primer coated panels: seven-day                     50 μm DFT exhibited more dense blisters            various metal substrates commonly used
  RT cure or one- to two-hour bake in a                     along the scribe line than the system              in some industrial coatings applications
  60°C oven. The final dry film thickness                   with 65 μm DFT, but the system with                that include aluminum alloys, stainless
  (DFT) of the waterborne primer films                      100 μm DFT showed no blisters. As                  steel, and galvanized steel. In general,
  after cure was around 55 to 80 μm. Test                   expected, higher film thickness provides           good adhesion, and therefore long-term
  panels were taped or coated on the back                   better and longer anti-corrosion protec-           corrosion protection to these substrates,
  and edges before being placed into the                    tion to metal substrates. In addition, the         could be difficult to achieve, especially
  Q-Lab Q-FOG chamber for ASTM B-117                        test results in this study suggest that the        with low-VOC formulations.
  test.                                                     impact of film thickness of waterborne                Figure 9 displays the panel images of
     Figure 7 shows the panel images of                     primer systems on anti-corrosion per-              MC #1, MC #2, and MC #3 systems over
  MC #1, MC #2, and MC #3 systems after                     formance could become more significant             aluminum alloy AA 2024 T3 substrates
  about 1000 h of salt-spray exposure and                   over sand-blasted steel panels. That is            after 2018 h, 1852 h, and 2018 h of
  after an 800-grit sandpaper was used to                   probably because waterborne primer sys-            salt-spray exposure, respectively. (The
  remove surface rust stains. Those films                   tems tend to penetrate and settle in the           panel surfaces were sanded via 220-
  were applied over SA 2.5 sand-blasted                     bottom crevices of the rough surface of            grit sandpaper followed by an acetone
  steel substrates with about 60 to 75 μm                   sand-blasted steel panels, which results           rinse and paper towel cleaning.) It can
  DFT. It can be seen that only some small                  in some weak areas with much lower film            be seen that MC #1 and MC #3 systems
  blisters formed near the scribe lines of                  thickness where corrosion can start.               exhibited excellent protection properties
  the WB-A system, and the coating still                       Figure 8 exhibits the panel images of           with only a few very tiny blisters formed
  has very good adhesion to the steel sub-                  MC #1, MC #2, and MC #3 systems after              along the scribe line after 2018 h of salt-
  strate along the X-shaped scribe lines.                   about 1000 h of salt-spray exposure and            spray exposure; the MC #2 system also
  The WB-B system has smaller blisters                      after removal of surface rust stains with          presented good anti-corrosion proper-
  in comparison to the WB-A system, but                     an 800-grit sandpaper. Those waterborne            ties with no blisters and delamination
  that might be due to 200 h less salt-                     primer systems were applied on CRS pan-            after 1800 h of salt-spray exposure
  spray exposure time. The COM system                       els with DFT of about 75 μm. Blisters were         on the panel field, though some small
  also shows good anti-corrosion perfor-                    only observed along the scribe lines for all       blisters formed along the scribe line. Wet
  mance, with very few blisters formed                      three systems, but the adhesion of coating         adhesion was measured on the test pan-
  on the film surface, but some creeps                      films to CRS substrates along the scribe           els (top right side of each panel) that had
  observed along the scribe lines.                          lines was not excellent; some underneath           been exposed in the salt spray chamber

FIGURE 8—Panel images of WB-A/MC #1, WB-B/MC #2, and COM/MC #3                 FIGURE 9—Panel images of WB-A/MC#1, WB-B/MC #2, and COM/MC #3 systems after 2018 h,
systems after 1162 h, 949 h, and 1162 h of salt-spray exposure, respectively   1852 h, and 2018 h of salt-spray exposure, respectively (AA 2024 T3 substrate, bake cure,
(S-36 type CRS substrate, bake cure, DFT ≈ 75 μm).                             DFT ≈ 65 μm).

        WB-A                       WB-B                         COM                       WB-A                          WB-B                          COM

                                                                                                                                PAINT.ORG |                   23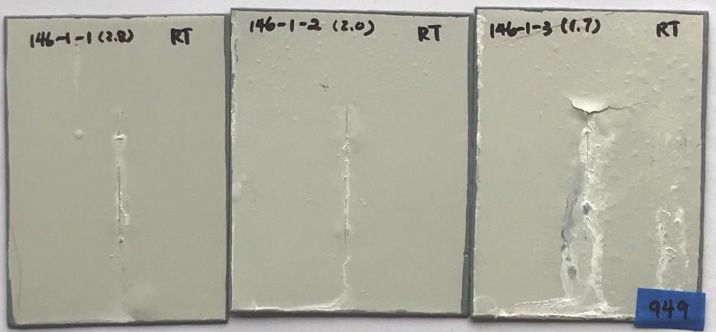
NOVEL CASHEW NUTSHELL LIQUID-BASED WATERBORNE CURING AGENTS

to endure the continuous attacks of ions               that in comparison to other substrates            for more than 800 h. It can be seen that
and water for more than 800 h; there-                  evaluated in this study, the blisters             MC #1 and MC #2 primer systems had
fore, the excellent wet cross-hatch adhe-              formed on galvanized steel panels were            very good dry adhesion regardless of the
sion observed from three primer systems                much more severe for similar duration             type of metal substrate used; after being
over AA 2024 T3 indicates excellent                    of salt-spray exposure. Even though gal-          exposed to salt spray for more than 800
long-term corrosion protection.                        vanized steel was the most challenging            h, the wet adhesion of MC #1 and MC #2
   The panel images of MC #1, MC #2,                   substrate, MC #1 and MC #3 systems                systems over aluminum alloy substrate
and MC #3 systems applied over stainless               still exhibited fairly good wet adhesion          was still excellent. Over stainless steel
steel substrates after about 1000 h of                 performance and could be good options             substrate, MC #1 system still maintained
salt-spray exposure are shown in Figure                for formulators. Some formulation                 excellent wet adhesion while MC #2
10. There were no blisters or delamina-                study to improve the corrosion protec-            system showed a little drop to 3B. Both
tion observed for the three systems.                   tion on galvanized steel substrate is             MC #1 and MC #2 systems still achieved
   Furthermore, MC #1, MC #2, and                      reported in Part III.                             3B wet adhesion over bare CRS. The
MC #3 systems were also applied over                      Table 4 summarizes the dry and wet             major difference in performance between
galvanized steel substrates that were                  cross-hatch adhesion of MC #1 and MC              MC #1 and MC #2 systems was observed
simply wiped with acetone. Figure                      #2 primer systems over four types of              when applying over galvanized steel sub-
11 displays the panel images of those                  metal substrates: nonpretreated bare CRS          strates: MC #1 system still provided good
systems after about 1000 h of salt-spray               with a smooth mill finish, galvanized             wet adhesion of 4B, but MC #2 system
exposure: MC#1 system had two to                       steel wiped with acetone, AA 2024 T3              lost adhesion after long salt-spray expo-
three large blisters and medium dense                  panels sanded via 220-grit sandpaper              sure. The test results in Table 4 demon-
blisters with size of 6 to 8 along the                 followed by acetone rinse and wiped, and          strate that the two new waterborne sam-
scribe line; MC #2 system showed two                   stainless steel with no surface prepa-            ples could provide excellent dry and wet
large blisters and some blisters with                  ration. The dry adhesion values were              adhesion over various metal substrates,
size of 8 along the scribe line; and MC                obtained on the cured panels that were            except MC #2 system showed poor wet
#3 system formed much larger and                       not exposed to salt spray, while the wet          adhesion over galvanized steel substrate.
denser blisters from the center scribe                 adhesion values were measured on panels           The excellent adhesion properties of new
line to both sides. Results demonstrate                after exposure in the salt spray chamber          waterborne samples could further benefit
                                                                                                         the long-term corrosion protection of
                                                                                                         different metal substrates.
              FIGURE 10—Panel images of WB-A/MC #1, WB-B/MC #2, and COM/MC #3 systems
              after 996 h, 949 h, and 996 h of salt-spray exposure, respectively (stainless              Part III: Wet-on-Wet Properties
              steel substrate, RT cure, DFT ≈ 65 μm).
                                                                                                         Quick self-recoat or recoatability with
                       WB-A                    WB-B                        COM                           PU coatings is a highly desirable prop-
                                                                                                         erty in industrial applications, such as
                                                                                                         transportation coatings, agricultural,
                                                                                                         construction and earth-moving equip-
                                                                                                         ment coatings, and rail car coatings.
                                                                                                         Very short recoat intervals between the
                                                                                                         application of primer and the next coat-
                                                                                                         ing layer are required, such as 30 min or
                                                                                                         less at RT or elevated cure conditions.
                                                                                                         Since the primer may not be fully dried
                                                                                                         when the next coat is applied, this cure
                                                                                                         process is usually called wet-on-wet
                                                                                                         application. If a primer system is slow
                                                                                                         in cure or has poor compatibility with
                                                                                                         PU topcoat, it will most probably result
FIGURE 11—Panel images of WB-A/MC#1, WB-B/MC #2, and COM/MC #3 systems after 1115 h, 949 h, and 1115 h
                                                                                                         in a dieback issue, which means that
of salt-spray exposure, respectively (galvanized steel substrate, RT cure, DFT ≈ 65 μm).
                                                                                                         the cured PU topcoat no longer has its
                                                                                                         original high gloss and may show poor
             WB-A                               WB-B                                COM                  adhesion to the primer system.
                                                                                                            The wet-on-wet topcoat performances
                                                                                                         were evaluated on the MC #4 system
                                                                                                         based on WB-A curing agent and Resin
                                                                                                         3; the MC #4 primer system had VOC of
                                                                                                         less than 75 g/L. The primer system was
                                                                                                         applied via air spray over CRS substrate
                                                                                                         at a wet film thickness of 50 to 65 μm.
                                                                                                         The test panels were set up in six groups:
                                                                                                         the panels in Groups #1 to #3 were cured
                                                                                                         at RT for 15, 30, and 45 min, respectively.
                                                                                                         Meanwhile, the panels in Groups #4 to

24                   | MAY 2020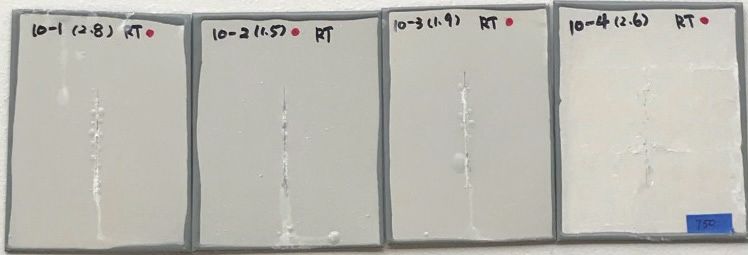
#6 were baked in a 60°C oven for 15, 30,      TABLE 4—Dry and Wet Adhesion of WB-A, WB-B, and COM Systems Over Various Metal Substrates
and 45 min, respectively. Subsequently, a                                                                   CROSS-HATCH ADHESION
commercial 2K solventborne PU system                SYSTEMS
was applied over all six groups of panels                                                                       GALVANIZED                                         STAINLESS
                                                                            ADHESION TYPE               CRS                     AA 2024 T3
                                                                                                                   STEEL                                             STEEL
via air spray. After a 24-h RT cure, the
glosses of the PU top-coated panels,                                              Dry                    5B         5B              5B                                 5B
                                                MC #1/WB-A
as well as their adhesions between the                                            Wet                    3B                   4B                     5B               5B
primer and PU topcoat, were measured                                              Dry                    5B                   5B                     5B               5B
and are listed in Table 6. Photo images of      MC #2/WB-B
those panels after cross-hatch adhesion                                           Wet                    3B                   0B                     5B               3B
tests are shown in Figure 12. Those test
results reveal that MC #4 system could        TABLE 5—Waterborne Primer Formulations Based on WB-A
maintain high gloss retention (>98%)
and excellent adhesion (5B) to the                             COMPONENTS                                  MC #4                 MC #5               MC #6           MC #7
commercial PU topcoat regardless of             WB-A                                                          5.51                 6.18               5.47            5.95
the cure conditions and recoat intervals.       Dispersant (Disperbyk 192)                                    0.09                 0.09               0.08            0.09
Furthermore, panels from Group #1 to
#3 were tested in salt spray for 881 h, and     Rheological additive (BENTONE SD-2)                           0.11                 0.12               0.10            0.11
they showed no blisters on field and had        Defoamer (BYK1640)                                            0.08                 0.09               0.08            0.08
creeps along scribe lines of less than 2        Pigment 1 (Ti-Pure R-706)                                     3.62                 3.87               3.42            3.72
mm (shown in Figure 13). The wet-on-
wet applied panels confirmed that the           Pigment 2 (Cimbar EX Barium Sulfate)                          7.97                 8.50               7.52            8.19
adhesion between MC #4 and PU top-              Inhibitor 1 (HALOX SW-111)                                    6.52                 6.96               6.15            6.70
coat was excellent even after a long time       Inhibitor 2 (HALOX 550WF)                                     0.49                 0.53               0.46            0.51
of salt spray testing. These combined test
results suggest that WB-A systems are           Filler 1 (Zeeospheres G 200)                                  4.35                 4.64               4.10            4.47
suitable for industrial coating appli-          Filler 2 (WOLLASTOCOAT 10 ES)                                 8.70                 9.28               8.20            8.93
cations due to their quick wet-on-wet           Filler 3 (Mica WG-325)                                        0.51                 0.54               0.48            0.52
properties and excellent long-term cor-
rosion protection performance.                  Solvent 1 (DOWANOL PM)                                        1.74                 1.86               1.64            1.79
                                                Solvent 2 (DPnB)                                              0.29                 0.31               0.27            0.30
Part IV: Formulation Study                      Flash rust inhibitor (HALOX Flash-X 150)                      0.22                 0.23               0.20            0.22
In this study, the influences upon              Water                                                       11.24                  11.98             10.59           11.54
anti-corrosion performance of changing
                                                Subtotal of Part A                                         51.44                   55.16             48.75           53.11
some factors in formulations, such as
varying solid epoxy dispersions, using          Resin 3                                                     39.14                      –                  –          37.21
different stoichiometric ratios, or adding      Resin 4                                                        –                   34.79                  –            –
different co-solvents, were evaluated.
                                                Resin 5                                                        –                       –             42.36             –
   In waterborne coating formulations,
good compatibility between solid epoxy          Water                                                         9.42                 10.05              8.89            9.68
dispersion and waterborne curing agent          Subtotal of Part B                                         48.56                   44.84             51.25           46.89
is critical for good overall performance.
                                                Total Part A & B                                          100.00                100.00               100.00         100.00
In this study, three primer systems, MC
#4, MC #5, and MC #6, were formulated           VOC (g/L)                                                   72.87                  75.96             66.72           75.24
at very comparable pigment composi-             wt% NVM                                                     57.14                  58.89             56.97           57.33
tion and PVC, at similar solids % and
co-solvent content, and by using the            wt% Pigment                                                 31.68                  33.78             29.86           32.52
same waterborne curing agent WB-A at            vol% NVM                                                   45.00                   50.85             43.33           44.80
1.24 stoichiometric ratio. Only the solid       % PVC                                                      29.52                   28.28             28.40           30.68
epoxy dispersions were changed with
Resin 3, Resin 2, and Resin 5 being used        Epoxy/amine                                                   1.24                 1.24               1.24            1.10
for MC #4, MC #5, and MC #6 systems,
respectively. The test results revealed       TABLE 6—Gloss Retention of the Test Panels After Wet-on-Wet Application
that the primer systems of MC #4 (based
on Resin 3) and MC #5 (based on Resin                                                                     RT                                                60°C
                                                        GLOSS @ 60°
2) exhibited much better corrosion                                                      15 MIN           30 MIN           45 MIN            15 MIN        30 MIN     45 MIN
protections than the MC #6 system               Original gloss of PU    a
                                                                                         89.5             89.5             89.5               89.5          89.5      89.5
(based on Resin 5), regardless of the           Gloss of two-coat system                 88.6             88.6             88.4               88.8          88.1       88.7
types of metal substrate. For example,
the three panels shown in Figure 14,            Gloss retention                         99.0%            99.0%            98.8%              99.2%         98.4%      99.1%
representing MC #4, MC #5, and MC #6            Cross-hatch adhesion                      5B               5B               5B                 5B            5B         5B
systems from left to right, were applied      (a) Original gloss of PU: the gloss of the panel having only PU coating over bare CRS.

                                                                                                                                           PAINT.ORG |                     25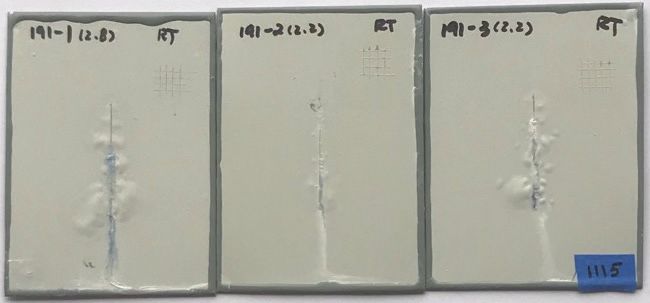
NOVEL CASHEW NUTSHELL LIQUID-BASED WATERBORNE CURING AGENTS

                                                     FIGURE 12—Photo images of the panels after wet-on-wet adhesion tests.

over galvanized steel substrate. After 750
h of salt-spray exposure, MC #4 and MC
#5 systems had some blisters along the
scribe lines, but no cracks or blisters on
the fields. However, the coating film of MC
#6 system became brittle, and some areas                  15 mins 60℃                   30 mins 60℃                       45 mins 60℃
started to show delamination from the
substrate. Those test results confirm that
choosing the proper solid epoxy dispersion
has significant effects on the final perfor-
mance of waterborne primer systems.
   Besides the epoxy resin selected, the
stoichiometric ratio between epoxy and
amine has a noticeable influence on the                     15 mins RT                    30 mins RT                        45 mins RT
overall properties of waterborne primer
systems. In our previous studies, 5,6 it was
found that the stoichiometric ratio of 1.25          FIGURE 13—Photo images of the wet-on-wet application panels after 881 h of salt-spray exposure.
gave the best performance when water-
borne primers were applied over blasted                      15 mins RT                     30 mins RT                     45 mins RT
or CRS substrates. Test results in Part II
confirmed that excellent long-term corro-
sion protection could be obtained for steel
substrates with 1.25 stoichiometric ratio
but was somehow worse over galvanized
steel substrate. Therefore, two primer
systems, MC #4 and MC #7, with different
“epoxy to amine” stoichiometric ratios
of 1.25 and 1.10, respectively, were tested
over galvanized steel substrates. After
750 h of exposure in salt spray chamber,
panels shown in Figure 15 suggested that
MC #7 system with stoichiometric ratio           FIGURE 14—Panel images of MC #4 system (left panel), MC #5 system (middle panel), and
of 1.10 exhibited better anti-corrosion          MC #6 system (right panel) after 750 h of salt-spray exposure (galvanized steel substrate,
performance than MC #4 due to much               RT cure, DFT ≈ 50–60 μm).
fewer blisters formed along the scribe
line. Results indicate that the increase
of WB-A use level in formulations could
effectively help to eliminate the blisters
over galvanized steel substrate.
   To achieve the low-VOC target of less than
75 g/L for waterborne primer systems, the
amount of co-solvent used in the formula-
tion was significantly reduced; subsequently,
the answer to “which types of co-solvents
could efficiently help with proper film
formation even at small use level?” became
important. In this study, five types of glycol
ether solvents were assessed through stor-
                                                                FIGURE 15—Panel images of MC #4 system (left panel) and MC #7
age stability, film appearance, and hiding
                                                                system (right panel) after 750 h of salt-spray exposure (galvanized
power. Those solvents are propylene glycol                      steel substrate, RT cure, DFT ≈ 50–60 μm).
monomethyl ether (PM), dipropylene glycol
n-butyl ether (DPnB), hexyl carbitol (HC),
propylene glycol propyl ether (PNP), and
propylene glycol phenyl ether (PPH). The
samples for storage stability tests were
prepared by mixing WB-A curing agent,
co-solvent, and DI water at 3:1:1 ratio, then
the samples were placed into a 50°C oven
for two months before any phase separation
was checked. For gloss measurement, the
panels were prepared by applying white
waterborne primers containing various

26                | MAY 2020
co-solvents over CRS panels. For the con-                   TABLE 7—Property Tests Using Different Solvents
trast ratio measurement, those waterborne
primers were applied over Leneta sealed                           TWO-MONTH STORAGE STABILITY @ 50°C OVEN                      GLOSS @ 60°               CONTRAST RATIO
black paper charts via drawdown after               PM                                 Good                                         29.6                        86.70
aging for 20 h at RT. After cure, contrast
ratio and gloss were measured using the             DPnB                 Little phase separation on surface                         14.4                        64.24
Datacolor Check II Plus and BYK Gardner             HC                   Little phase separation on surface                         15.3                        66.79
micro-TRI-gloss meter.
                                                    PNP                                Good                                         27.5                        86.03
   Table 7 shares storage stability, gloss,
and contrast ratio results. One can see             PPH                      Severe phase separation                                21.3                        75.31
that PM and PNP systems had no phase
separation at 50°C after two months,
which suggests that PM and PNP have              FIGURE 16—Panel images of five waterborne primer systems containing different co-solvents after a 20-h RT aging.
better compatibility with WB-A than
the other three solvent systems. Gloss
and contrast ratio data revealed similar
trends: the PM and PNP systems gave
higher glosses than the other three sol-
vent systems due to better film forma-
tion. PM and PNP systems gave higher
contrast ratios, which indicated those
two systems had better hiding power,
or ability to cover black background, as
observed in Figure 16. Since those five
primer systems were applied over Lene-
ta sealed black paper charts after 20-h
aging of waterborne paints at RT, the
better hiding power suggests that PM             enable short recoat intervals of 15 to                       Zhuhai, China for the new product
and PNP could possibly extend the pot            30 min for multi-layer coating systems                       developments.
life of waterborne primer systems based          to achieve excellent adhesion and
on WB-A and Resin 3.                             anti-corrosion properties, as well as to                     References
                                                 maintain aesthetic appearance.                               1. Lomonaco, D., Mele, G., and Mazzetto, S.E., Cashew
                                                    Furthermore, formulation studies that                        Nutshell Liquid (CNSL): From an Agro-industrial Waste to
CONCLUSIONS                                      varied solid epoxy dispersions, stoichio-                       a Sustainable Alternative to Petrochemical Resources,
In this article, a series of low-VOC             metric ratios, and co-solvents suggested                        Anilkumar, P. (Ed.), Springer International Publishing AG,
(
You can also read


