Developing Nanostructured Ti Alloys for Innovative Implantable Medical Devices - MDPI
←
→
Page content transcription
If your browser does not render page correctly, please read the page content below
materials
Review
Developing Nanostructured Ti Alloys for Innovative
Implantable Medical Devices
Ruslan Z. Valiev 1,2, *, Egor A. Prokofiev 2 , Nikita A. Kazarinov 2 , Georgy I. Raab 1 ,
Timur B. Minasov 3 and Josef Stráský 4
 1   Institute of Physics of Advanced Materials, Ufa State Aviation Technical University, 12 K. Marx street,
     450008 Ufa, Russia; giraab@mail.ru
 2   Laboratory of Mechanics of Advanced Bulk Nanomaterials, Saint Petersburg State University,
     Universitetskiy prospekt 28, Peterhof, 198504 St. Petersburg, Russia; egpro@mail.ru (E.A.P.);
     n.kazarinov@spbu.ru (N.A.K.)
 3   Department of Traumatology and Orthopedics, Bashkir State Medical University, 3 Lenin street, 450008 Ufa,
     Russia; m004@yandex.ru
 4   Department of Physics of Materials, Charles University, Ke Karlovu 3, 121 16 Prague, Czech Republic;
     josef.strasky@gmail.com
 *   Correspondence: ruslan.valiev@ugatu.su

 Received: 31 October 2019; Accepted: 14 February 2020; Published: 21 February 2020

 Abstract: Recent years have witnessed much progress in medical device manufacturing and the
 needs of the medical industry urges modern nanomaterials science to develop novel approaches for
 improving the properties of existing biomaterials. One of the ways to enhance the material properties
 is their nanostructuring by using severe plastic deformation (SPD) techniques. For medical devices,
 such properties include increased strength and fatigue life, and this determines nanostructured Ti
 and Ti alloys to be an excellent choice for the engineering of implants with improved design for
 orthopedics and dentistry. Various reported studies conducted in this field enable the fabrication of
 medical devices with enhanced functionality. This paper reviews recent development in the field of
 nanostructured Ti-based materials and provides examples of the use of ultra-fine grained Ti alloys
 in medicine.

 Keywords: nanostructured Ti alloys; severe plastic deformation; enhanced strength and fatigue life;
 medical implants with improved design; shape-memory NiTi alloy; functionality

1. Introduction
     Presently, Ti and its alloys represent the top choice when a combination of high strength, light
weight, and affordable cost are required, such as in the area of medical device manufacturing. However,
the clinical demands for implantable medical devices are growing rapidly, and nowadays new Ti
alloys are being investigated in terms of their chemical composition optimization, manufacturing
processes and modification of surface to meet the appropriate medical standards and comply with
regulation [1,2]. One possibility to design and manufacture new materials with enhanced properties
focuses on nanostructuring of metallic materials using the so-called severe plastic deformation
(SPD) techniques, which have become a cutting edge and promising area in materials science and
engineering [3,4].
     Different SPD techniques are applied to refine grains in metallic materials to below micrometer
range or even to the nanosized range. SPD techniques are also efficient for the formation of nanoclusters
and nanoprecipitates of secondary phases, enhancing the mechanical and functional properties of
the materials [4,5]. A whole variety of SPD techniques have been developed and put forward to
provide very high strains (ε > 5) under high applied pressure, such as accumulative roll bonding

Materials 2020, 13, 967; doi:10.3390/ma13040967                                 www.mdpi.com/journal/materials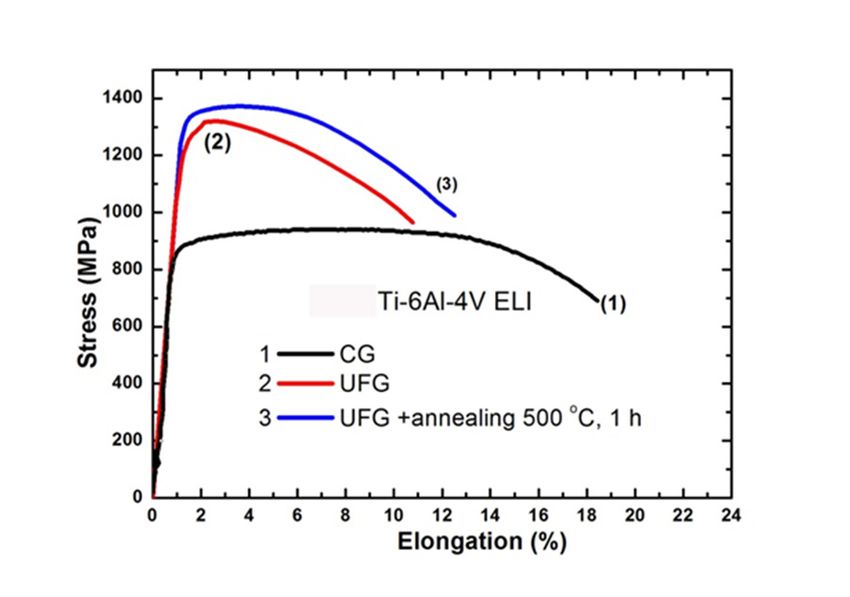
Materials 2020, 13, 967                                                                             2 of 16

(ARB), including multiple forging, twist extrusion, and others [6–8]. However, equal channel angular
pressing (ECAP) and high pressure torsion (HPT), introduced already in the pioneering works [3],
remain the most used methods for the production of ultrafine-grained (UFG) materials. Principles of
these techniques, developed devices and microstructure evolution during processing steps have been
thoroughly reviewed in numerous studies [3–7,9,10]. Recently, these deformation techniques have
been further upgraded for practical application [11,12].
     Nanostructuring of metallic materials increases material strength due to work hardening and
grain refinement [13,14], consequently, fatigue life can be also significantly increased by microstructure
refinement [15]. Understanding material processing by SPD techniques is essential for designing of
medical devices with improved functionality as it not only improves mechanical properties but also
affects corrosion and biomedical properties [16–18]. Improved strength and enhanced biomedical
response of a nanostructured material can be efficiently used in dental implants; a stent of such
permanent implant manufactured from nanostructured Ti can be significantly smaller due to the
increased strength and therefore less harmful for a patient [19].
     Recently, materials scientists have been exploring possibilities of improved interaction of
nanostructured materials with body tissues, for instance bones. In this respect, surface modifications of
bulk nanomaterials demonstrate encouraging results [17,18,20,21]. These improvements provide the
possibility for development and design of implantable medical devices that perform better and provide
improved functionality in comparison to their counterparts manufactured from common coarse-grained
materials. This review article outlines the progress in engineering of advanced nanostructured Ti alloys
and medical implants/devices manufactured from those advanced materials.

2. SPD Processing of Nanostructured Titanium Materials

2.1. Commercially Pure Ti
      The first studies devoted to Ti-based materials potentially applicable in medicine were applied to
commercial purity titanium (CP Ti) due to its high biocompatibility with living tissues [22]. Unparalleled
biocompatibility of Ti was the main interest of many clinical studies of medical devices and tools
applied in traumatology, orthopedics, and dentistry. Unfortunately, CP Ti is characterized by reduced
strength when compared to other metallic materials used in biomedical devices such as steels or
cobalt-based alloys. Achieving higher strength level is possible by alloying or thermo-mechanical
processing, but then the Ti-based materials usually lose their biometric response or fatigue performance.
Therefore, SPD processing was considered as an alternative strategy proving that nanostructuring of
CP Ti may become a novel approach to improve the mechanical properties of this material to achieve
its high-performance [13,17,19,20,23]. Apart from enhancing mechanical properties, this strategy
is also advantageous in improving the biological response of the surface of the CP titanium based
products [18,20].
      The first results on nanostructured CP Ti Grade 4 (O–0.34%, Fe–0.3%, C–0.052%, N–0.015%, all
in wt.%, balance–Ti] were achieved by Valiev et al. aiming on manufacturing rods with significantly
enhanced mechanical properties and superior biomedical response for the fabrication of dental
implants [19]. The processing route involved equal-channel angular pressing (ECAP) as an SPD
technique [9] followed by thermo-mechanical treatment by forging and, finally, drawing. Continuous
SPD processing by ECAP-Conform (ECAP-C) and subsequent drawing, was capable of producing rods
with the diameter of 7 mm and the length of 3 m with homogeneous ultrafine-grained (UFG) structure
along the entire length of the rods [23,24]. Furthermore, ECAP-Conform represents an economical
SPD-based fabrication procedure for mass production of ‘nanoTi’.
      After combined severe plastic deformation and thermo-mechanical processing, the grain size was
significantly reduced from 25 µm in the initial Ti rods to 150 nm in the processed material. Figure 1
illustrates the effect of ECAP-C strain on the density of high-angle boundaries (HAB) and mechanical
strength of CP Ti Grade 4 [21].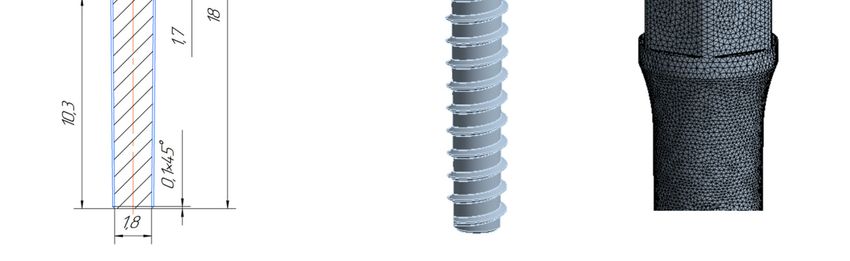
Materials 2020, 13, 967 3 of 16
Materials 2020, 13, 967 3 of 15
Figure1.1.Influence
Figure InfluenceofofECAP-C
ECAP-Cstrain onon
strain (a)(a)
grain boundary
grain (GB)
boundary density,
(GB) (b) yield
density, strength
(b) yield and (c)
strength andthe
(c)
contribution of various strengthening mechanisms [21].
the contribution of various strengthening mechanisms [21].
Table
Table11shows
showsthe
theimproved
improvedmechanical
mechanicalproperties
propertiesofofCP CPTiTiafter
afternanostructuring
nanostructuringby byECAP
ECAPandand
subsequent thermomechanical treatment. The strength of the nanostructured titanium
subsequent thermomechanical treatment. The strength of the nanostructured titanium is doubled is doubled when
compared to the conventional
when compared CP titanium.
to the conventional CP The increase
titanium. Thein increase
strength was achievedwas
in strength without reduction
achieved of
without
ductility (total elongation to failure is above the limit of 10%), which is otherwise commonly
reduction of ductility (total elongation to failure is above the limit of 10%), which is otherwise observed
after intensive
commonly drawing
observed or rolling.
after intensive drawing or rolling.
Table1.1.Mechanical
Table Mechanicalproperties
propertiesofofcoarse-grained
coarse-grained(CG)
(CG)and
andnanostructured
nanostructuredCP
CPGrade
Grade44Ti.
Ti.Annealed
Annealed
Ti-6Al-4V ELI (extra low interstitials) alloy for comparison.
Ti-6Al-4V ELI (extra low interstitials) alloy for comparison.
Fatigue
Reduction Fatigue
State Processing UTS, MPaUTS, YS, MPa
YS, Elongation,
Elongation, % Reduction Strength at
State Processing Area, % Strength at
MPa MPa % Area, % 106 Cycles
106 Cycles
1 Initial CG Ti 700 530 25 52 340
1 Initial CG Ti 700 530 25 52 340
2 2 nanoTinanoTi 1240 1240 1200
1200 1212 42 42 620 620
Annealed
Annealed
3 3 Ti-6Al-4V 940 840840 1616 45 45 530 530
Ti-6Al-4V ELI 940
ELI
Fatigue tests of conventional and nanostructured CP Ti were conducted in air at room
temperaturetests
Fatigue of conventional
in accordance withand nanostructured
ASTM E 466-96 with CP the
Ti were conducted
loading in airofat20
frequency roomHztemperature
and R = 0.1.
in accordance
Table 1 showswith thatASTM E 466-96
the fatigue with of
strength thenanoTi
loading frequency
[17,24] after of
one20million R = 0.1.
Hz andcycles Table 1doubled
is almost shows
that the fatigue strength of nanoTi [17,24] after one million cycles is almost
when compared to the conventional CP titanium and even exceeds the fatigue performance of the Ti-doubled when compared to
the conventional CP titanium and even exceeds the fatigue performance
6Al-4V alloy [22,25]. Significant enhancement of fatigue properties and improved strength of of the Ti-6Al-4V alloy [22,25].
Significant
nanostructuredenhancement
Ti allowof usfatigue properties
to produce smaller and improved
sizes strength
of implants andof nanostructured
therefore to reduce Tithe
allow us to
extent of
produce smaller sizes of implants
a surgical intervention (see also Section 3). and therefore to reduce the extent of a surgical intervention (see also
Section CP3).Ti is known for its considerable biocompatibility which results from the presence of the
CP Ti is
protective known
oxide film.for its considerable
Titanium dioxide TiO biocompatibility
2 forms naturally which
on theresults
surfacefrom
of CPtheTipresence of the
and represents
protective oxide film. Titanium dioxide
a stable protective layer on that a mineralized TiO 2 forms naturally on the surface of CP Ti and
bone matrix can be attached. This film is usually 5–represents a
stable
10nmprotective
thick andlayer on that a inert,
biologically mineralized
thus itbone matrixacan
prevents be attached.
potentially This film
negative is usually
reaction 5–10nm
between the
thick and biologically inert, thus it
surrounding body environment and the metal [22].prevents a potentially negative reaction between the surrounding
body NanoTi
environment withand UFG thestructure
metal [22]. containing high density of non-equilibrium grain boundaries
NanoTi
achieved bywith
SPDUFG structure
is also containing
characterized by high density of
significantly non-equilibrium
increased internal grain
energy boundaries achieved
of the material [3].
by SPD is also characterized by significantly increased internal energy of
This fact may result in considerable change in the morphology of the oxide film on the materialthe material [3]. This fact may
result in considerable
surface. NanoTi with change in thesurface
polished morphology of the
exhibits oxide filmbiological
improved on the material surface.
reaction of theNanoTi
surfacewithas
polished
confirmed surface exhibits
by recent improved
studies biological
in a series reaction of
of experiments the surface
through as confirmed tests
cytocompatibility by recent
usingstudies
mouse
in a series of
fibroblast experiments
cells [20,26–29].through
At the cytocompatibility
same time, additional tests using mouse fibroblast
improvement cells [20,26–29].
of biomedical propertiesAtof
the same time, additional
nanostructured titanium improvement
can be achieved of biomedical
by dedicated properties
surface of modifications
nanostructuredsuch titanium can be
as chemical
achieved by dedicated surface
etching or bioactive coatings [17,18]. modifications such as chemical etching or bioactive coatings [17,18].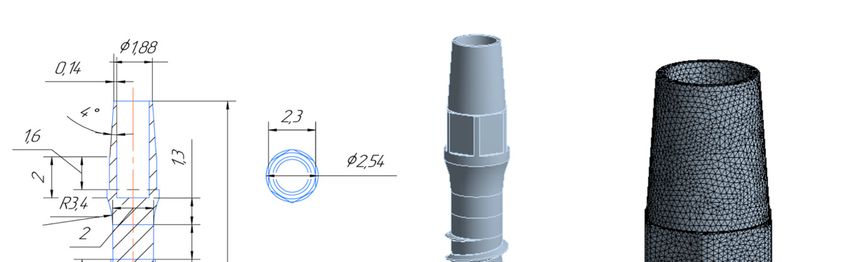
Materials  2020,13,
 Materials2020,  13,967
                     967                                                                                        44 ofof1615

 2.2. Titanium Alloys
2.2. Titanium Alloys
       Two-phase (α + β) titanium alloys such as Ti-6Al-4V and Ti-6Al-7Nb continue to be the most
      Two-phase (α + β) titanium alloys such as Ti-6Al-4V and Ti-6Al-7Nb continue to be the most
 important metallic materials in the dental and orthopedic fields due to their excellent mechanical
important metallic materials in the dental and orthopedic fields due to their excellent mechanical
 properties and satisfactory biocompatibility [2,22,30,31].
properties and satisfactory biocompatibility [2,22,30,31].
       Several recent studies reported improved mechanical and functional properties of
      Several recent studies reported improved mechanical and functional properties of nanostructured
 nanostructured titanium alloys.
titanium alloys.
       Microstructure and mechanical properties of Ti-6Al-4V ELI (extra low interstitial alloys for
      Microstructure and mechanical properties of Ti-6Al-4V ELI (extra low interstitial alloys for medical
 medical applications) prepared by SPD are reported in [15,32,33]. Round rods of the two-phase alloy
applications) prepared by SPD are reported in [15,32,33]. Round rods of the two-phase alloy with
 with the diameter of 40 mm (Intrinsic Devices Company, San Francisco, CA, USA) and with chemical
the diameter of 40 mm (Intrinsic Devices Company, San Francisco, CA, USA) and with chemical
 composition: Ti–base, Al–6.0%; V–4.2%; Fe–0.2%; О–0.11%; N–0.0025%; Н–0.002%, С–0.001 (wt.%)
composition: Ti–base, Al–6.0%; V–4.2%; Fe–0.2%; O–0.11%; N–0.0025%; H–0.002%, C–0.001% (wt.%)
 had the grain size of about 8 µm in a cross-section and 20 µm in a longitudinal section. X-ray
had the grain size of about 8 µm in a cross-section and 20 µm in a longitudinal section. X-ray diffraction
 diffraction analysis proved that the volume fractions of α and β phases were approximately 85% and
analysis proved that the volume fractions of α and β phases were approximately 85% and 15%,
 15%, respectively. 250 mm length rods were processed in two steps. The rods were subjected to ECAP
respectively. 250 mm length rods were processed in two steps. The rods were subjected to ECAP via
 via route Bc at 600 °С and subsequently extruded, altogether with total strain of 4.2 [33]. The extrusion
route Bc at 600 ◦ C and subsequently extruded, altogether with total strain of 4.2 [33]. The extrusion
 steps were carried out at 300 °С with the last pass at room temperature for additional strengthening.
steps were carried out at 300 ◦ C with the last pass at room temperature for additional strengthening.
 The rods with the diameter of 18 mm and length up to 300 mm were produced. The rods were finally
The rods with the diameter of 18 mm and length up to 300 mm were produced. The rods were finally
 annealed in the temperature range from 200 °С to 800 °С for 1 h and subsequently cooled in air.
annealed in the temperature range from 200 ◦ C to 800 ◦ C for 1 h and subsequently cooled in air.
       Transmission electron microscopy (TEM) studies showed that SPD leads to a complex UFG
      Transmission electron microscopy (TEM) studies showed that SPD leads to a complex UFG
 structure containing refined grains and subgrains with a mean size of about 300 nm.
structure containing refined grains and subgrains with a mean size of about 300 nm.
       Stress–strain curves for the initial coarse-grained and UFG material shown in Figure 2
      Stress–strain curves for the initial coarse-grained and UFG material shown in Figure 2 demonstrate
 demonstrate that the alloy after grain refinement by SPD underwent significant strengthening.
that the alloy after grain refinement by SPD underwent significant strengthening. Tensile elongation of
 Tensile elongation of the UFG material (curve 2) is reduced from 17% to 9%. Strength/ductility trade
the UFG material (curve 2) is reduced from 17% to 9%. Strength/ductility trade off, however, improved
 off, however, improved after subsequent annealing at 500 °С. The results of tensile tests correspond
after subsequent annealing at 500 ◦ C. The results of tensile tests correspond to the measurement of
 to the measurement of microhardness [32,33].
microhardness [32,33].

      Figure 2. Engineering stress−strain tensile curves of the Ti-6Al-4V ELI alloy: coarse-grained material
      (initial)
        Figure(1);   UFG condition
                 2. Engineering     (2) and UFG
                                stress−strain    condition
                                              tensile curvesafter annealing
                                                             of the            500 ◦alloy:
                                                                            at ELI
                                                                    Ti-6Al-4V        C (3).coarse-grained material
        (initial) (1); UFG condition (2) and UFG condition after annealing at 500 °С (3).
      In accordance with [10], enhancement of the ductility in the UFG material by annealing is clearly
associated  with a decrease
       In accordance           of internal
                        with [10],         elasticof
                                   enhancement      stress  and dislocation
                                                      the ductility          density.
                                                                    in the UFG          Simultaneous
                                                                                  material by annealing additional
                                                                                                           is clearly
strengthening   of the  alloy can  be explained   by the  observed  decrease   in content  of metastable
 associated with a decrease of internal elastic stress and dislocation density. Simultaneous additional    β-phase
after  cooling from
 strengthening         the
                  of the    annealing
                         alloy          temperature.
                               can be explained    by theIts volumedecrease
                                                           observed    fraction in
                                                                                 incontent
                                                                                     the UFG    alloy annealed
                                                                                            of metastable         at
                                                                                                            β-phase
500 ◦
 afterCcooling
         can be higher
                from the than  before annealing,
                            annealing   temperature.as shown   in [10],
                                                        Its volume       due toinquenching
                                                                     fraction                 fromannealed
                                                                                  the UFG alloy     the annealing
                                                                                                               at 500
temperature.    Despite  no  visible particles of any  secondary   phase,   aging
 °С can be higher than before annealing, as shown in [10], due to quenching from theprocesses  might  have  caused
                                                                                                          annealing
grain  boundaryDespite
 temperature.     segregations   associated
                           no visible        with
                                      particles of additional  improvement
                                                   any secondary                of the
                                                                     phase, aging      properties
                                                                                     processes     of the
                                                                                                might     annealed
                                                                                                       have  caused
UFG    material [34].
 grain boundary segregations associated with additional improvement of the properties of the
 annealed UFG material [34].
Materials 2020, 13, 967 5 of 16
Materials 2020, 13, 967 5 of 15
Finetuning
Fine tuningofofmechanical
mechanicalproperties
propertiesby byannealing
annealingafter
afterthe
theSPD
SPDprocessing
processingisislimited
limitedmainly
mainlyby by
grain growth occurring at elevated temperatures. Thermal stability of UFG structure
grain growth occurring at elevated temperatures. Thermal stability of UFG structure of commercially of commercially
pure Ti
pure Ti follows
follows classical
classical grain
grain growth
growth depending
depending on on temperature
temperature via via Arrhenius
Arrhenius equation
equation [35]
[35] and
and
limited to approximately 450 ◦ C [36]. Nanostructured α + β exhibit enhanced thermal stability up to
limited to approximately 450 °C [36]. Nanostructured α + β exhibit enhanced thermal stability up to
◦ C [37].
550°C
550 [37].
Fatigue properties
Fatigue properties ofofthe
theTi-6Al-4V
Ti-6Al-4V ELIELI
alloyalloy
withwith
UFG UFGstructure were investigated.
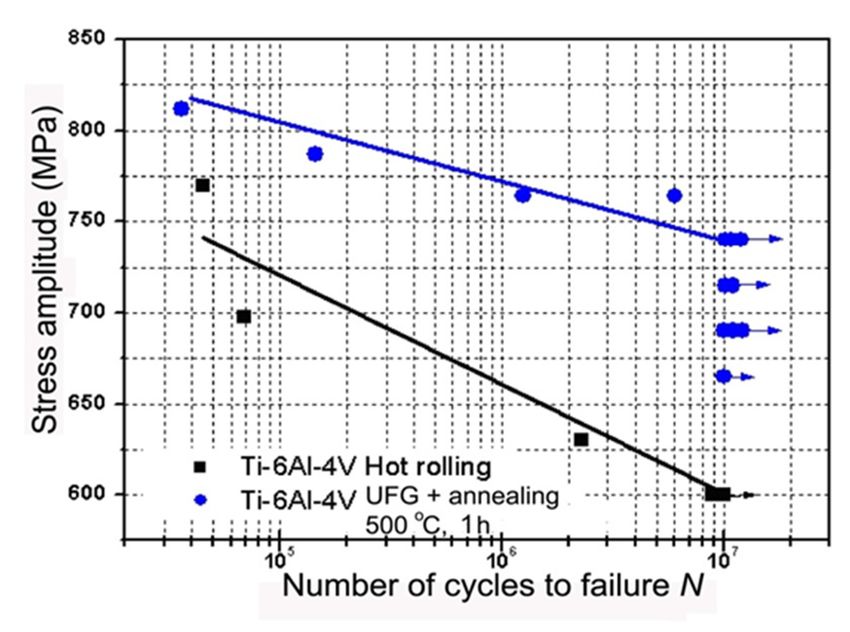
structure High strength
were investigated. High
and enhanced ductility (1370 MPa and 12%) after SPD processing and subsequent
strength and enhanced ductility (1370 МPа and 12%) after SPD processing and subsequent annealing annealing at 500 ◦ C;
resulted
at 500 °С in an enhancement
resulted of fatigue
in an enhancement oflimit to 740
fatigue MPa
limit after
to 740 МPа107after
cycles
107incycles
comparison to 600 MPa
in comparison in
to 600
the initial coarse-grained condition (Figure 3) [32].
МPа in the initial coarse-grained condition (Figure 3) [32].
Figure 3. Fatigue test results of initial coarse-grained material and UFG material after annealing at
500 ◦ C,3.1 Fatigue
Figure h. test results of initial coarse-grained material and UFG material after annealing at
500 °С, 1 h.
The fatigue limit of the Ti-6Al-4V alloy in UFG condition reported in [32] tested by rotating
bending
The was slightly
fatigue limithigher
of thethan the values
Ti-6Al-4V in [32,38]
alloy in UFGproving thatreported
condition measuredinfatigue properties
[32] tested depend
by rotating
on the choice of the measurement technique.
bending was slightly higher than the values in [32,38] proving that measured fatigue properties
depend Achieved results of
on the choice show
the that high strength
measurement can be achieved in UFG Ti-6Al-4V ELI alloy by processing
technique.
by ECAP and subsequent
Achieved results show thermo-mechanical
that high strengthtreatment. SelectioninofUFG
can be achieved SPD Ti-6Al-4V
regimes and ELIadjustment
alloy by
processing by ECAP and subsequent thermo-mechanical treatment. Selection of SPD regimes us
of processing parameters of SPD processing such as temperature, strain rate and strain allow andto
manipulateofthe
adjustment grain boundary
processing parametersstructure
of SPD and phase morphology
processing in the two-phase
such as temperature, UFGand
strain rate alloy. As
strain
the result,
allow us to the best combination
manipulate the grain of strengthstructure
boundary and ductility can bemorphology
and phase achieved along with
in the the improved
two-phase UFG
fatigue
alloy. Asendurance
the result,limit. Enhancement
the best combination of of
strength
strength and ductility
and ductilityof the
can biomedical
be achievedTi-6Al-7Nb
along withalloy the
was reported
improved in another
fatigue endurance comprehensive study [39].
limit. Enhancement of In comparison
strength to Ti-6Al-4V,
and ductility of thethe Ti-6Al-7Nb
biomedical alloy
Ti-6Al-
represents
7Nb alloy wasa better
reportedchoice for biomedical
in another use duestudy
comprehensive to avoiding the toxic vanadium
[39]. In comparison [40]. the
to Ti-6Al-4V, This study
Ti-6Al-
shows
7Nb that
alloy processing
represents by ECAP
a better andfor
choice consequent
biomedicalthermo-mechanical
use due to avoidingtreatment
the toxic causing
vanadium formation
[40]. This of
UFG structure
study shows that results in high strength
processing by ECAP (1400andMPa) and ductility
consequent (elongation of 10%).
thermo-mechanical These achieved
treatment causing
propertiesof
formation areUFG
attractive for designing,
structure developing
results in high and manufacturing
strength(1400 of high-performance
MPa) and ductility (elongation ofmedical
10%).
devicesachieved
These and implants.
properties are attractive for designing, developing and manufacturing of high-
Considering
performance medical that vanadium
devices and partly also aluminum are rather toxic elements and,
and implants.
simultaneously,
Considering that that reducing
vanadiumofand the partly
Young’s alsomodulus
aluminum is required
are ratherfortoxic avoiding
elements so-called
and,
stress-shielding that
simultaneously, [39], reducing
the development of brandmodulus
of the Young’s new biomedical alloysfor
is required represents
avoidingaso-called
current relevant
stress-
challenge [39],
shielding for researchers. A new generation
the development of brand of newtitanium alloys must
biomedical alloysprovide improved
represents strength,
a current better
relevant
biocompatibility,
challenge and lower
for researchers. A Young’s modulusofthan
new generation Ti6Al4V
titanium alloy.
alloys Current
must research
provide focuses
improved on new
strength,
alloying
better systems, in particular
biocompatibility, and lowerTi-Nb and Ti-Mo.
Young’s modulus than Ti6Al4V alloy. Current research focuses on
Given the
new alloying above mentioned
systems, requirements,
in particular Ti-Nb and Ti-Mo.the interest is drawn to titanium alloys containing high
content
Givenof the phase,mentioned
theβabove because this phase is characterized
requirements, the interest byislower
drawn Young’s modulus
to titanium in the
alloys range of
containing
high content of the β phase, because this phase is characterized by lower Young’s modulus in the
range of 55–90 GPa, and thus exhibit lower stress shielding [39,41–43]. Moreover, these Ti alloys are
Materials 2020, 13, 967 6 of 16
Materials 2020, 13, 967 6 of 15
55–90 GPa, and thus exhibit lower stress shielding [39,41–43]. Moreover, these Ti alloys are designed
designed
to containtoonly
contain only non-toxic
non-toxic constituentsconstituents
such as Nb, suchMo, asZr,
Nb,and
Mo, Zr,On
Ta. andtheTa. On hand,
other the other hand,
these these
materials
materials are characterized by comparatively low strength, because the
are characterized by comparatively low strength, because the lowest Young’s modulus is obtainedlowest Young’s modulus is
obtained only in treated
only in solution solutionsingle
treated single
phase phase
β-Ti β-TiAchieving
alloys. alloys. Achieving
low Young’slow Young’s
modulusmodulus
and highand high
strength
strength simultaneously
simultaneously is a challenging
is a challenging task. Ageing task. Ageing treatments
treatments that inducethata fineinduce a fine and
and uniform uniform
precipitation
precipitation
of ω and α phaseof ω components
and α phaseprovides
components provides
significant significant strengthening.
strengthening. On the other hand, On the other
this hand,
inevitably
this inevitably
increases increases
the Young’s the Young’s
modulus modulus
of the alloy [41–43].of the
Onlyalloy [41–43].present
few studies Only few studiesresults
successful presentin
successful results in development of thermal treatments without detrimental
development of thermal treatments without detrimental effect on some of the relevant mechanical effect on some of the
relevant
propertiesmechanical
[44,45]. properties [44,45].
Advancements
Advancements ininthethe areas
areas of orthopedics
of orthopedics and dentistry
and dentistry called forcalled for newforstrategies
new strategies development for
development of new generation of β-Ti alloys with reduced Young’s modulus
of new generation of β-Ti alloys with reduced Young’s modulus and high strength, which would be more and high strength,
which
suitable would be more
for such suitableRecently,
applications. for such SPDapplications.
processing Recently,
has beenSPD processing
proposed has been
to fabricate proposed to
nanocrystalline
fabricate
β-Ti alloys nanocrystalline β-Ti alloys
with high strength, with highofstrength,
low modulus elasticitylow andmodulus
excellentofbiocompatibility
elasticity and excellent
[46–51].
biocompatibility [46–51]. Nanostructuring of these alloys leads to improved
Nanostructuring of these alloys leads to improved strength due to grain refinement and substructure strength due to grain
refinement and In
evolution [52]. substructure
particular, evolution [52]. Inβ-Ti
solution treated particular,
Ti15Mosolution treated
alloy, which β-Ti Ti15Mo
is qualified for alloy,
medical which
use,
is qualified for medical use, can be significantly refined by HPT as demonstrated
can be significantly refined by HPT as demonstrated in Figure 4a. Grain size can be decreased well in Figure 4a. Grain
size
below can100
benm
decreased well below
[53]. Significant 100 nm [53].apart
disadvantage, Significant disadvantage,
from limited size of HPTapartsamples,
from limited size of
is formation
HPT samples, is induced
of deformation formation ωof deformation
phase causing induced ω phaseofcausing
sharp increase sharp increase
elastic modulus [54]. of elastic modulus
Subsequent aging
[54]. Subsequent aging of UFG Ti15Mo alloy leads to two-phase α +
of UFG Ti15Mo alloy leads to two-phase α + β structure which is also characterized by increased β structure which is also
characterized by increased
modulus of elasticity modulus
[55–57]. of elasticity
More promising is [55–57]. More promising
using Ti-Nb-Ta-Zr based is usingwhich
alloys Ti-Nb-Ta-Zr
are less based
prone
alloys which are less prone to ω phase formation. Ti-29Nb-13Ta-5Zr alloy prepared
to ω phase formation. Ti-29Nb-13Ta-5Zr alloy prepared by HPT exhibited increased yield stress from by HPT exhibited
increased
550 to 800 yield
MPa withstressunchanged
from 550 elastic
to 800 modulus
MPa with[58,59]. unchanged elasticmicrostructure
Significant modulus [58,59]. Significant
refinement was
microstructure refinement
recently also achieved was recently also
in Ti-35Nb-6Ta-7Zr achieved in
biomedical Ti-35Nb-6Ta-7Zr
alloy by ECAP (Figure biomedical
4b). alloy by ECAP
(Figure 4b).
(a) (b)
Figure 4. Microstructure
Figure 4. Microstructureofof
(a)(a) Ti15Mo
Ti15Mo alloy
alloy prepared
prepared by and
by HPT HPT(b)and (b) Ti-35Nb-6Ta-7ZZr
Ti-35Nb-6Ta-7ZZr alloy
alloy prepared
prepared
by ECAP by ECAP (cross-section).
(cross-section).
Microstructural refinement
Microstructural refinement in in β-Ti alloys can
β-Ti alloys can be
be also
also enhanced
enhanced by by multiple
multiple twinning
twinning and/or
and/or
martensitic transformation
martensitic transformationβ β →→ α’’α” [60].
[60]. The nanocrystalline
The nanocrystalline β-Ti alloys
β-Ti alloys also display
also display excellentexcellent
in vitro
in vitro biocompatibility
biocompatibility as shownas shown by enhanced
by enhanced cell cell attachment
attachment andand proliferation[48].
proliferation [48].These
These novel
novel
nanocrystalline β-Ti
nanocrystalline β-Tialloys
alloyshave
havehigh chances
high to meet
chances the challenge
to meet of next-generation
the challenge implant material
of next-generation implant
with significant
material prospectsprospects
with significant in load bearing
in loadbiomedical applications.
bearing biomedical applications.
2.3. Nanostructured
2.3. Nanostructured NiTi
NiTi Shape
Shape Memory
Memory Alloys
Alloys
NiTi alloys
NiTi alloysexhibit unique
exhibit mechanical
unique behavior—shape
mechanical memory effect
behavior—shape (SME)effect
memory and superelasticity,
(SME) and
which arise from a transformation between martensite and austenite phases [61,62]. NiTi alloys
superelasticity, which arise from a transformation between martensite and austenite phases are
[61,62].
NiTi alloys are important materials which are already used in advanced medical devices due to the
above mentioned mechanical properties and, additionally, due to functional properties such as good
biocompatibility and corrosion resistance in vivo [61,63]. At the same time, new, advanced
responsible for the shape memory effect [65,66]. During following thermal treatments nanocrystalline
(NC) structure can be obtained in NiTi alloys via crystallization process (Figure 5) [64,67].
Nanocrystalline NiTi alloys with grain size about 20 nm demonstrate very high strength up to 2000
MPa [64].
      Equal
Materials 2020,channel
                13, 967    angular pressing is another SPD processing technique applied for producing                       7 of 16
uniform UFG structure in bulk NiTi alloys. The ECAP processing of NiTi at 400–450 °C results in
formation of UFG structure with grain size of about 200 nm (Figure 5).
important
      UFG materials
               structure which     are already
                            formation      leads used     in advanced
                                                    to significant         medical devices
                                                                       improvement              due to the above
                                                                                           of mechanical       and mentioned
                                                                                                                      functional
mechanical      properties   and,  additionally,     due  to functional    properties   such   as
properties of NiTi-based alloys [64,68–70]. The ultimate tensile strength (UTS) of UFG NiTi alloy good   biocompatibility     and
corrosion
attains     resistance
          1400            in vivois[61,63].
                 MPa, which          50% higherAt thethan
                                                      sameintime,
                                                                CG new,    advanced
                                                                     alloys;   and theapplications
                                                                                           yield stresswill  require
                                                                                                          (YS)         enhanced
                                                                                                                increases    after
properties     (higher   strength,  higher     recovery    strain and   stress,  etc.)  of  NiTi
ECAP from 500 MPa to 1100 MPa (Figure 6a). The functional shape-memory effect of NiTi after ECAP  shape   memory     alloys.
      During
is also  improvedthe past   two6b).
                       (Figure    decades,     there hascompletely
                                      The maximum          been interest     in the application
                                                                          recoverable               of increases
                                                                                          strain εrmax SPD methods  fromto6% NiTi
                                                                                                                               (in
alloys
CG       because
     state)  to 9%the    formation
                      after ECAP and  of nanocrystalline
                                          the maximum recoveryand UFGstressstructures
                                                                                  σrmax allows
                                                                                        reachesenhancing
                                                                                                   1120 MPa,mechanical        and
                                                                                                                 which is twice
functional
more   than theproperties
                   level ofinCGcomparison
                                  alloys (about  to coarse
                                                    500 MPa) grained   materials
                                                                [69]. UFG           [63,64].
                                                                              structure    formation in Ni-rich NiTi alloys
      HPT      processing     of  NiTi   alloys     leads   to  a  transformation
by ECAP results in an emergence of superelasticity at temperature close                  from    crystalline
                                                                                                        to thetohuman
                                                                                                                    amorphous
                                                                                                                            body
phase.     Microstructural       changes      in  deformed     NiTi    during    thermal     treatment
temperature. Superelasticity in UFG NiTi is characterized by a narrow mechanical hysteresis and            are of  key   interest
                                                                                                                              low
as they are
residual        responsible
           strain   [71].       for the shape memory effect [65,66]. During following thermal treatments
nanocrystalline      (NC) structure
      The high-strength        NC and  canUFGbe obtained    in NiTi
                                                   NiTi alloys       alloys
                                                                  with        via crystallization
                                                                         improved      functionalprocess      (Figure 5)
                                                                                                     characteristics      [64,67].
                                                                                                                        are  very
Nanocrystalline        NiTi   alloys   with    grain   size  about    20  nm    demonstrate
promising for medical applications in particular for manufacturing of stents, embolic protection  very   high   strength   up to
2000 MPa
filters, guide[64].
                  wires, and other peripheral vascular devices (see Section 4).

                                 (a)                                                            (b)
      Figure 5. Microstructure
                Microstructure of
                               of (a)
                                   (a)NC
                                      NCand
                                         and(b)
                                             (b)UFG
                                                UFGNiTi
                                                    NiTialloys
                                                         alloysprocessed
                                                                processedby
                                                                          byHPT
                                                                            HPTand
                                                                                andECAP,
                                                                                    ECAP,respectively.
                                                                                          respectively.

     Equal channel angular pressing is another SPD processing technique applied for producing
uniform UFG structure in bulk NiTi alloys. The ECAP processing of NiTi at 400–450 ◦ C results in
formation of UFG structure with grain size of about 200 nm (Figure 5).
     UFG structure formation leads to significant improvement of mechanical and functional properties
of NiTi-based alloys [64,68–70]. The ultimate tensile strength (UTS) of UFG NiTi alloy attains 1400 MPa,
which is 50% higher than in CG alloys; and the yield stress (YS) increases after ECAP from 500 MPa
to 1100 MPa (Figure 6a). The functional shape-memory effect of NiTi after ECAP is also improved
(Figure 6b). The maximum completely recoverable strain εr max increases from 6% (in CG state) to 9%
after ECAP and the maximum recovery stress σr max reaches 1120 MPa, which is twice more than the
level of CG alloys (about 500 MPa) [69]. UFG structure formation in Ni-rich NiTi alloys by ECAP results
in an emergence of superelasticity at temperature close to the human body temperature. Superelasticity
in UFG NiTi is characterized by a narrow mechanical hysteresis and low residual strain [71].
     The high-strength NC and UFG NiTi alloys with improved functional characteristics are very
promising for medical applications in particular for manufacturing of stents, embolic protection filters,
guide wires, and other peripheral vascular devices (see Section 4).
Materials 2020, 13, 967 8 of 16
Materials 2020, 13, 967 8 of 15
(a) (b)
Mechanical
Figure6.6.Mechanical
Figure properties
properties of NiTi
of NiTi alloyalloy
in CGincondition
CG condition andECAP.
and after after ECAP. (a) Engineering
(a) Engineering stress–
stress–strain
strain curves
curves for fortests
tensile tensile testsstate
in CG in CG
(1)state (1) and
and after afterusing
ECAP ECAP using
4 (2), 4 (2),
8 (3) and812(3)(4)
and 12 (4)and
passes passes
(b)
and (b) functional properties (ε max and σ max ) as a function of number of ECAP passes [61].
functional properties (εr and σ
max
r r ) as a function
max
r of number of ECAP passes [61].
3.3.Design
Designof ofMiniaturized
MiniaturizedImplantsImplants
Enhanced mechanical
Enhanced mechanicalproperties
properties of nanostructured
of nanostructured metals allowallow
metals development of medical
development of implants
medical
with better design, for instance with a more subtle design which is
implants with better design, for instance with a more subtle design which is less harmful for less harmful for human body
human[17].
Application
body [17]. of stronger nanostructured CP Ti instead of common CG Ti, allows for altering the
design of devices.ofRecently,
Application strongerdetailed computations
nanostructured CP Ti were
insteadconducted
of common to analyze
CG Ti, the possible
allows geometries
for altering the
of miniplates for maxillofacial surgery manufactured from nanostructured
design of devices. Recently, detailed computations were conducted to analyze the possible Ti [72].
CP Ti of
geometries miniplate
miniplates specified by ASTMsurgery
for maxillofacial F 67, manufactured
was considered fromby nanostructured
Conmet Company (Moscow,
Ti [72].
Russia) as the benchmark for redesigning the product dimensions of
CP Ti miniplate specified by ASTM F 67, was considered by Conmet Company (Moscow, Russia) mini-plates manufactured from
nanostructured CP Ti. The mechanical properties in a cross-section
as the benchmark for redesigning the product dimensions of mini-plates manufactured from of a newly designed plate were
calculated with CP
nanostructured the Ti.
useTheof estimates
mechanical of the fatigue performance
properties in a cross-sectionlimit for
of acoarse-grained
newly designed Grade
plate4 were
CP Ti
and nanostructured Grade 4 CP Ti. In practical use, the mini-plates are
calculated with the use of estimates of the fatigue performance limit for coarse-grained Grade 4 CP subjected to bending loads,
therefore
Ti bending strength
and nanostructured Grade of 4mini-plates from conventional
CP Ti. In practical and nanostructured
use, the mini-plates are subjected CPtoTibending
was compared.
loads,
The result bending
therefore indicates strength
that the plate from nanostructured
of mini-plates Ti has significantly
from conventional improved bending
and nanostructured CP strength
Ti was
and therefore,
compared. Theitresult
is clearly advantageous
indicates that theoverplatethefrom
standard device currently
nanostructured Ti hasmanufactured
significantly from CG Ti.
improved
bendingRecently,
strengththree-dimensional
and therefore, finite it is element models (FEM) over
clearly advantageous were the
developed
standard using CAEcurrently
device software
(KOMPAS-3D v15,
manufactured from CG Ti. ASCON Group, Saint Petersburg, Russia) and then imported into ANSYS Workbench
18.2 Recently,
(ANSYS Inc., Canonsburg, PA,
three-dimensional USA)
finite [73] for
element geometry
models (FEM)analysis of nanoTiusing
were developed dental CAEimplants.
software In
addition to static
(KOMPAS-3D v15,strength,
ASCONcalculations
Group, Saint of virtual fatigueRussia)
Petersburg, testing were carried
and then out using
imported theANSYS
into built-in
fatigue module. For all tested models, mesh sensitivity testing was
Workbench 18.2 (ANSYS Inc, Canonsburg, Pennsylvania, U.S.A.) [73] for geometry analysis of nanoTi performed in order to obtain
mesh-independent results.
dental implants. In addition to static strength, calculations of virtual fatigue testing were carried out
usingThe the following procedure
built-in fatigue was used
module. to assess
For all tested possible
models,ways meshtosensitivity
miniaturize the implants.
testing The device
was performed in
with a standard geometry was
order to obtain mesh-independent results. assumed to be made from the conventional coarse-grained CP Ti. The
model Thewas designed
following in a way was
procedure to obtain
usednearly critical
to assess stressways
possible state toboth in terms ofthe
miniaturize static and fatigue
implants. The
failure. Afterwards, the same loading was applied to a model with
device with a standard geometry was assumed to be made from the conventional coarse-grained reduced dimensions but with CPthe
properties of nano CP Ti.
Ti. The model was designed in a way to obtain nearly critical stress state both in terms of static and
fatigueA failure.
one-stage dental implant
Afterwards, the samewithloading
genericwasgeometry
appliedwas to aconsidered
model withinreduced
the study. The shape
dimensions butof
the implant is similar to
with the properties of nano CP Ti. the implant geometry produced from nano CP Ti by company Timplant s.r.o.
(Ostrava, Czech Republic)
A one-stage [74]. Figure
dental implant with 7generic
shows ageometry
technical was
drawing of the geometry
considered of thisThe
in the study. nanoimplant
shape of
with a corresponding numerical model.
the implant is similar to the implant geometry produced from nano CP Ti by company Timplant s.r.o.
(Ostrava, Czech Republic) [74]. Figure 7 shows a technical drawing of the geometry of this
nanoimplant with a corresponding numerical model.Materials
Materials
Materials 2020,
2020, 13,
13,13,
2020, 967
967967 9 of
9 9of of 15
1615
(a)
(a) (b)
(b) (c)
(c)
Figure
Figure 7.
7. 7.
Figure Geometry
Geometry
Geometry of
ofof the
the
the dental
dental
dental nanoimplant:
nanoimplant: (a)
(a)(a)
nanoimplant: technical
technical drawing
drawing
technical with
with
drawing dimensions
dimensions
with in
inin
dimensions mm;mm; (b)
(b)(b)
mm; 3D
3D3D
model;
model; (c) (c) enlarged
enlarged FEM
FEM mesh.
mesh.
model; (c) enlarged FEM mesh.
TheThe
Theapplied
applied
applied loading scheme
loading
loading was inspired
scheme
scheme was by theby
was inspired
inspired testing
by procedures
the testing
the used in the
testing procedures
procedures ISOin
used
used 14801
in the standard.
the ISO 14801
ISO 14801
The performed
standard. The
standard. calculations
The performed revealed
performed calculations that application
calculations revealed
revealed that of the nanoTi
that application
application of allows
of the reduction
the nanoTi
nanoTi allows of the diameter
allows reduction
reduction ofof the
the
ofdiameter
implant by
diameter of at least
implant 10%,
by at while
least 20%
10%, diameter
while 20% reduction
diameter leads to
reduction an unacceptable
leads to an decrease
unacceptable
of implant by at least 10%, while 20% diameter reduction leads to an unacceptable decrease of the
decrease
device’s
of the fatigue
of the device’sstrength.
device’s fatigue Maximal
fatigue strength. principal
strength. Maximalstress
Maximal zonestress
principal
principal for thezone
stress implant
zone with
for the
for the diameter
the implant
implant reduced
with the
with by
the diameter
diameter
10% loaded
reduced by
reduced with
by 10% a 67.75
10% loaded N force
loaded with is shown
with aa 67.75
67.75 N in
N forceFigure
force is 8.
is shown
shown in in Figure
Figure 8.
8.
Figure
Figure Maximal
8. 8.
Figure principal
8. Maximal
Maximal stress
principal
principal for the
stress
stress forUFG
for Ti implant
the UFG
the UFG with awith
Ti implant
Ti implant 10%areduced
with a 10% diameter
10% reduced
reduced and 67.75
diameter
diameter and
andN 67.75
force.
67.75 NN
force.
force.
4. Fabrication and Tests of Medical Nanoimplants
4. Fabrication
4. Fabrication and Tests
Tests of
Recently, manufacturing
and of Medical
Medical Nanoimplants
and successful testing of several medical implants fabricated from
Nanoimplants
nanostructured Ti have been
Recently, manufacturingconsidered
manufacturing and successful[17].
in detail
and successful Another
testing example
of several
several of the innovative
medical development
implants fabricated
fabricated from
Recently, testing of medical implants from
is nanostructured
the manufacturing Ti and
havetesting
been of the implant
considered inpins designed
detail [17]. for surgery
Another in the
example bone
of tissue
the of the
innovative
nanostructured Ti have been considered in detail [17]. Another example of the innovative
hip, which increases
development thebone
is the strength and
manufacturing andprevents
testing ofitsthe
of fracture
implant(Figure 9) [75]. The
pins designed
designed pins of two
for surgery
surgery types
in the
the bone
development is manufacturing and testing the implant pins for in bone
tissue of the hip, which increases bone strength and prevents its fracture (Figure 9) [75].
tissue of the hip, which increases bone strength and prevents its fracture (Figure 9) [75]. The pins of The pins ofMaterials 2020, 13, 967 10 of 16
Materials 2020, 13, 967 10 of 15
Materials 2020, 13, 967 10 of 15
two types
(Figure 10)(Figure 10) were from
were produced produced from nanostructured
nanostructured Ti rods of Ti 3 mmrodsdiameter
of 3 mm with diameter verywith
highvery high
strength
two
(σ types
strength
= 1300 (σ (Figure
= 1300
MPa). 10)
MPa).
These were produced
These were
implants implants from
usedwerenanostructured
to studyusedtheir
to study Ti rods
effecttheir
on theof 3
effectmm
boneon diameter
the bone
strength with very
of strength high
of the
the hip, which
strength
hip, which (σ =
was1300 MPa).
evaluated These
by implants
means of were
bench used
testing to study
[76]. For their
this
was evaluated by means of bench testing [76]. For this purpose, a special device (Figure 11) was usedeffect
purpose, on the
a bone
special strength
device of the
(Figure
hip,
to which
11)analyze
was used was
the to evaluated
analyze the
mechanical by means
mechanical
properties of bench testing
properties
of implant [76].
of implant
systems For this
under systems purpose,
compression a
underalong special device
compression
the axis of (Figure
along the
the hip.
11)
axiswas
Such of used
the
systems hip.to Such
wereanalyze the mechanical
systems
subjected towere
a defined properties
subjectedload to of
theimplant
a defined
along axis load systems
along
of the hip,the under
as axis of
well compression
as the hip,
in the as along
well asthe
perpendicular in
axis
the of the hip.
perpendicular Such systems
direction were
with a subjected
force to
directed a defined
to the load
region along
of the
direction with a force directed to the region of the greater trochanter to complete fracture at a rate ofthe axis
greater of the hip,
trochanter as
to well as
complete in
5the perpendicular
fracture
mm/min atusing
a ratethedirection
of 5 mm
INSTRON with /a force
5982 min directed
using High
(Instron®, to the
the region of
INSTRON
Wycombe, the greater
5982 trochanter
(Instron®,
Buckinghamshire, High
UK) toWycombe,
complete
multipurpose
fracture
one at a rateUK)
Buckinghamshire,
pin dynamometer. ofAmultipurpose
5total
mm of 3/ systems
min oneusing
pin the INSTRON
weredynamometer.
studied: threeA 5982
total
pins, a of (Instron®,
3 systems
spiral, and a were High
spiral Wycombe,
studied:
+ pin three
system.
Buckinghamshire,
pins, a spiral, and UK)
a multipurpose
spiral + pin system. one pin
As a dynamometer.
result [76], the A
use total
of of 3 systems
different
As a result [76], the use of different implants demonstrated high efficiency in improving the strength of were
implants studied: three
demonstrated
pins,
bone aefficiency
spiral,
high tissue in and
the a spiral
in hip.
improving + pinthesystem.
In particular, strength
the useAsofof
a bone
result [76],
tissue
a spiral and the usehip.
ina the
pin of the
in different implants
In bone-implant
particular, demonstrated
thesystem
use of made
a spiralit
high
and aefficiency
pin in thein improving
bone-implant the strength
system made of bone
it tissue
possible toin the
increase hip.the
possible to increase the axial load resistance by 72.6% in comparison to the tests excluding implants. In particular,
axial load the use
resistance of a
by spiral
72.6%
and
This ademonstrated
pin in the to
in comparison bone-implant
the prospect
the system
tests excluding made itofpossible
implants.
of integration toreinforcement
increase the the
This demonstrated
surgical axial load
prospect
of the resistance
hip made by 72.6%
of integration
of nano CP Tiof
in
intocomparison
surgical to the
reinforcement
clinical practice to tests
of theexcluding
prevent hip implants.
madebones.
broken of nano CP This demonstrated
Ti into clinical practicethe prospect
to prevent of broken
integration
bones.of
surgical reinforcement of the hip made of nano CP Ti into clinical practice to prevent broken bones.
Figure 9. The image of the hip after the insertion of reinforcing implants.
Figure
Figure 9. The image
9. The image of
of the
the hip
hip after
after the
the insertion
insertion of
of reinforcing
reinforcing implants.
implants.
(a)
(a)
(b)
(b)
Figure 10.
Figure 10. Two
Twotypes
typesof
ofthe
theimplant
implantsystems
systemsused:
used: ((a)
((a) aa pin;
pin; (b)
(b) aa spiral)
spiral) and
and their
their application
application using
using
Figure
the 10.
INSTRONTwo types
5982 of the implant
dynamometer.
the INSTRON 5982 dynamometer. systems used: ((a) a pin; (b) a spiral) and their application using
the INSTRON 5982 dynamometer.Materials 2020, 13, 967 11 of 16
Materials 2020, 13, 967 11 of 15
Figure
Figure 11. Testing
Testing procedure of the reinforced hip sample.
interesting example
Another interesting exampleofofthe theinnovative
innovativeapplication
application is the
is the removable
removable clipping
clipping device
device for
for blood vessels, tubular structures, and soft tissues fabricated from UFG
blood vessels, tubular structures, and soft tissues fabricated from UFG NiTi with enhanced shape- NiTi with enhanced
shape-memory
memory effectdesigned
effect and and designed for bleeding
for bleeding control control
duringduring laparoscopic
laparoscopic operations.
operations. This This device
device has
has been
been created
created andand tested
tested in collaboration
in collaboration between
between UfaUfa State
State AviationTechnical
Aviation TechnicalUniversity
University(USATU)
(USATU)
and National University of Science and Technology Technology “MISIS”
“MISIS” [24].
[24].
The conducted tests demonstrated that the removable removable clipping devices produced from UFG NiTi NiTi
alloy obtain several advantages when compared to the standard counterpart. Table
obtain several advantages when compared to the standard counterpart. Table 2 provides the 2 provides the most
important
most properties
important of the clipping
properties device for
of the clipping the UFG
device andUFG
for the conventional CG alloy. The
and conventional CG maximum
alloy. The
opening angle
maximum of theangle
opening jaws, of
at which no residual
the jaws, at whichdeformation
no residual was observed,was
deformation increases 160◦ , which
up toincreases
observed, up
is significantly higher than that of benchmark CG alloy. The value of the reversible
to 160°, which is significantly higher than that of benchmark CG alloy. The value of the reversible shape memory
effect (up
shape to 4 mm)
memory and(up
effect the to
maximum
4 mm) and ratedthe
force that develops
maximum rated at triggering
force the clipping
that develops device (upthe
at triggering to
0.9 N) also
clipping doubles
device (up in
to the
0.9 product from UFG
N) also doubles alloys.
in the product from UFG alloys.
Table 2.
Table Service characteristics
2. Service characteristics of
of the
the clipping
clipping device
device produced
produced from
from the
the NITi
NITi alloys.
alloys.
Material
Opening Angleofof
Opening Angle the Opening of the
Opening Jaws
of the atatReversible
Jaws Reversible Max
MaxRated
Rated Force ofthe
Force of the
Material ◦
theJaws,
Jaws, ° Shape
Shape Memory
Memory Effect,mm
Effect, mm Clipping Device,
Clipping Device, HН
CG
CGMaterials 2020, 13, 967 12 of 16
and formation of secondary phase precipitations allows for considerable improvement of the strength
and fatigue properties. In the present paper the advantages of nanostructuring were demonstrated for
CP Ti, Ti alloys including new β-Ti alloys as well as the NiTi alloy with shape memory effect. The
approaches to computer design of a number of miniaturized medical implants made from high-strength
nanomaterials have been suggested. In addition, the paper includes the examples of manufacturing
and tests of selected advanced medical devices for traumatology and surgery from Ti nanobiomaterials.
Taking into account the results of recent studies on surface modification, including chemical etching
of nanometals and deposition of bioactive coatings, it is assumed that the developments of Ti-based
nanomaterials opens new possibilities for advanced medical implants and devices with improved
design and functionality.
Author Contributions: R.Z.V. introduced the concept and contents of the present paper, together with co-authors
conducted the analysis and description of the resulting data. E.A.P. prepared the results of studies on the structure
and properties of UFG TiNi alloy with shape memory effect. N.A.K. provided the results of the design of
miniaturized implants (Section 3). G.I.R. provided the description of SPD techniques for processing CP Ti and Ti
alloys to produce UFG structure. T.B.M. introduced the original data on manufacturing and testing of the implant
pins designed for surgery in the bone tissue of the hip. J.S. reviewed the results of studies on biomedical Ti alloys
subjected to SPD processing. All authors have read and agreed to the published version of the manuscript.
Funding: This research was funded by Russian Science Foundation grant № 19-49-02003 and by Ministry of
Education, Youth and Sports of the Czech Republic (project №LTARF18010). The authors gratefully acknowledge
the financial support from Saint Petersburg State University in the framework of Call 3 project (id 26130576 for
R.Z.V., E.A.P. and N.A.K.). This work was also financially by Ministry of Industry and Trade of the Czech Republic
(project № FV20147).
Conflicts of Interest: The authors declare no conflict of interest.
References
1. Hanawa, T. Overview of metals and applications. In Metals for Biomedical Devices; Elsevier BV: Amsterdam,
The Netherlands, 2010; pp. 3–24.
2. Froes, F.H.; Qian, M. Titanium in Medical and Dental Applications, 1st ed.; Woodhead Publishing: Duxford,
UK, 2018.
3. Valiev, R.; Islamgaliev, R.; Alexandrov, I. Bulk nanostructured materials from severe plastic deformation.
Prog. Mater. Sci. 2000, 45, 103–189. [CrossRef]
4. Valiev, R.Z.; Estrin, Y.; Horita, Z.; Langdon, T.G.; Zehetbauer, M.J.; Zhu, Y.T. Producing bulk ultrafine-grained
materials by severe plastic deformation: Ten years later. JOM 2016, 68, 1216–1226. [CrossRef]
5. Valiev, R.Z.; Estrin, Y.; Horita, Z.; Langdon, T.G.; Zehetbauer, M.J.; Zhu, Y.T. Fundamentals of superior
properties in bulk nanoSPD materials. Mater. Res. Lett. 2016, 4, 1–21. [CrossRef]
6. Whang, S.H. Nanostructured Metals and Alloys: Processing, Microstructure, Mechanical Properties and Applications,
1st ed.; Woodhead Publishing Limited: Cambridge, UK, 2011.
7. Rosochowski, A. Severe Plastic Deformation Technology; Whittles Publishing: Scotland, UK, 2017.
8. Estrin, Y.; Vinogradov, A. Extreme grain refinement by severe plastic deformation: A wealth of challenging
science. Acta Mater. 2013, 61, 782–817. [CrossRef]
9. Valiev, R.Z.; Langdon, T.G. Principles of equal-channel angular pressing as a processing tool for grain
refinement. Prog. Mater. Sci. 2006, 51, 881–981. [CrossRef]
10. Rack, H.J.; Qazi, J.; Allard, L.; Valiev, R.Z. Thermal Stability of Severe Plastically Deformed VT-6 (Ti-6Al-4V).
Mater. Sci. Forum 2008, 584, 893–898. [CrossRef]
11. Takizawa, Y.; Masuda, T.; Fujimitsu, K.; Kajita, T.; Watanabe, K.; Yumoto, M.; Otagiri, Y.; Horita, Z. Scaling
up of High-Pressure Sliding (HPS) for Grain Refinement and Superplasticity. Met. Mater. Trans. A 2016, 47,
4669–4681. [CrossRef]
12. Fakhretdinova, E.I.; Raab, G.I.; Valiev, R.Z. Modeling of Metal Flow during Processing by
Multi-ECAP-Conform. Adv. Eng. Mater. 2015, 17, 1723–1727. [CrossRef]
13. Valiev, R.Z. Nanostructuring of metals by severe plastic deformation for advanced properties. Nat. Mater.
2004, 3, 511–516. [CrossRef]You can also read


